


Recent Projects
U.S. Pharmaceutical Solid Dosage ISO 8 Modular Cleanroom Project
2026-06-23


Airkey successfully delivered a modular cleanroom solution for a pharmaceutical R&D laboratory in Melbourne, Australia. Designed to meet strict GMP requirements while providing flexibility for future expansion, the cleanroom offers a highly controlled environment for pharmaceutical research and product development.
| Item | Details |
|---|---|
| Project Name | Australia Pharma R&D Clean Lab |
| Industry | Pharmaceutical R&D |
| Location | Melbourne, Australia |
| Cleanroom Class | ISO 8 (Class 100,000) |
| Cleanroom Area | 37.6 m² |
| Internal Height | 3.0 m |
| Product Model | Light Series (FAG-I9N-A63 (9×7)-F) |
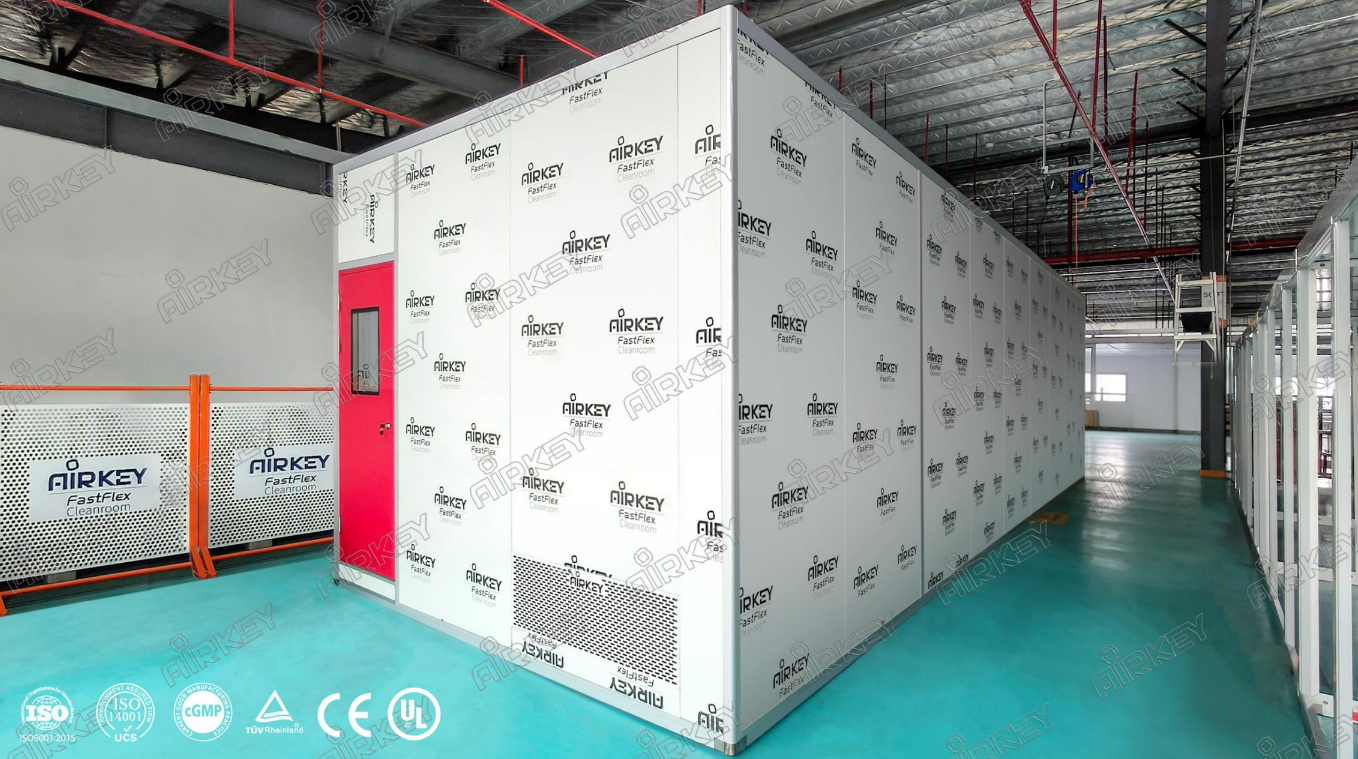
Established in 2011, Oak Laboratories Pty Ltd. is an Australian company specializing in product development services for the pharmaceutical, veterinary, cosmeceutical, and food industries.
With extensive expertise in formulation development and manufacturing, the company required a cleanroom environment that could support diverse R&D activities while complying with stringent pharmaceutical regulations.
The client required a cleanroom solution capable of:
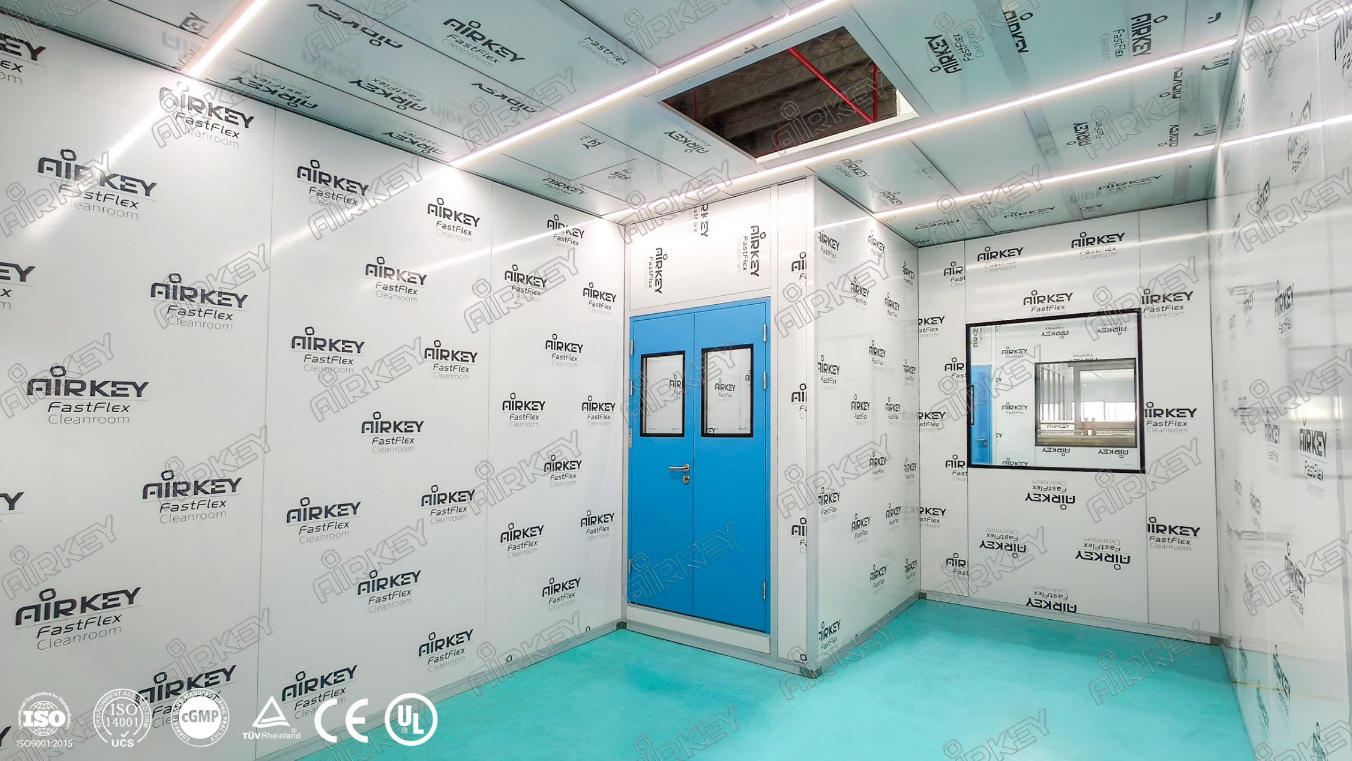
To address the client's requirements, Airkey designed and supplied a modular ISO 8 cleanroom featuring:
The cleanroom was designed, manufactured, and validated in accordance with pharmaceutical GMP standards, ensuring compliance with stringent regulations applicable to pharmaceutical, veterinary, cosmetic, and food industries.
Considering the client's evolving R&D needs, the cleanroom adopts a modular design that allows easy reconfiguration and future expansion, minimizing downtime and investment costs.
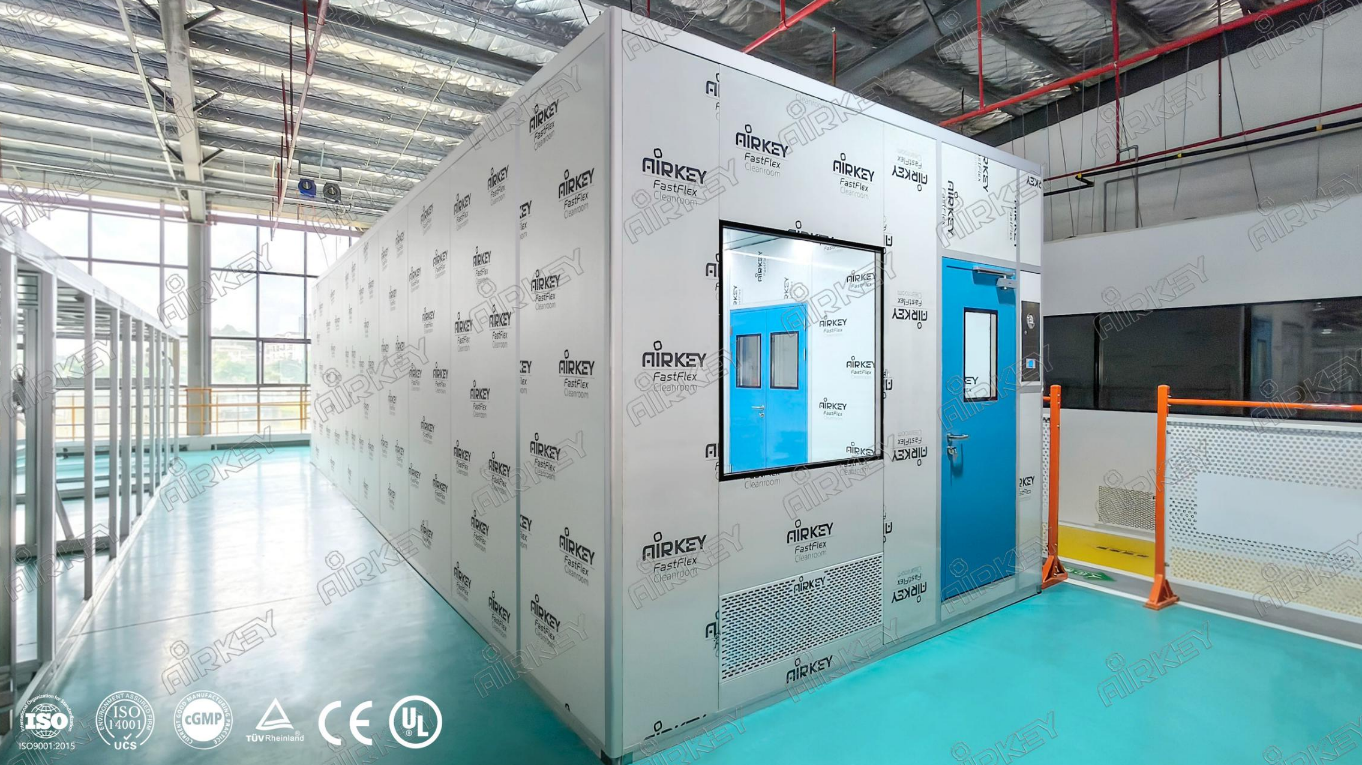
All wall panels, structural frames, and interior materials are resistant to disinfectants and chemical corrosion. Smooth, non-porous surfaces and rounded joints help prevent particle accumulation and facilitate easy cleaning.
The cleanroom utilizes H14 HEPA filtration combined with EC FFUs to provide stable airflow and effective particle control, ensuring ISO 8 cleanliness performance.
Factory prefabrication combined with on-site assembly significantly reduced installation time by approximately 40–60% compared with conventional cleanroom construction methods.
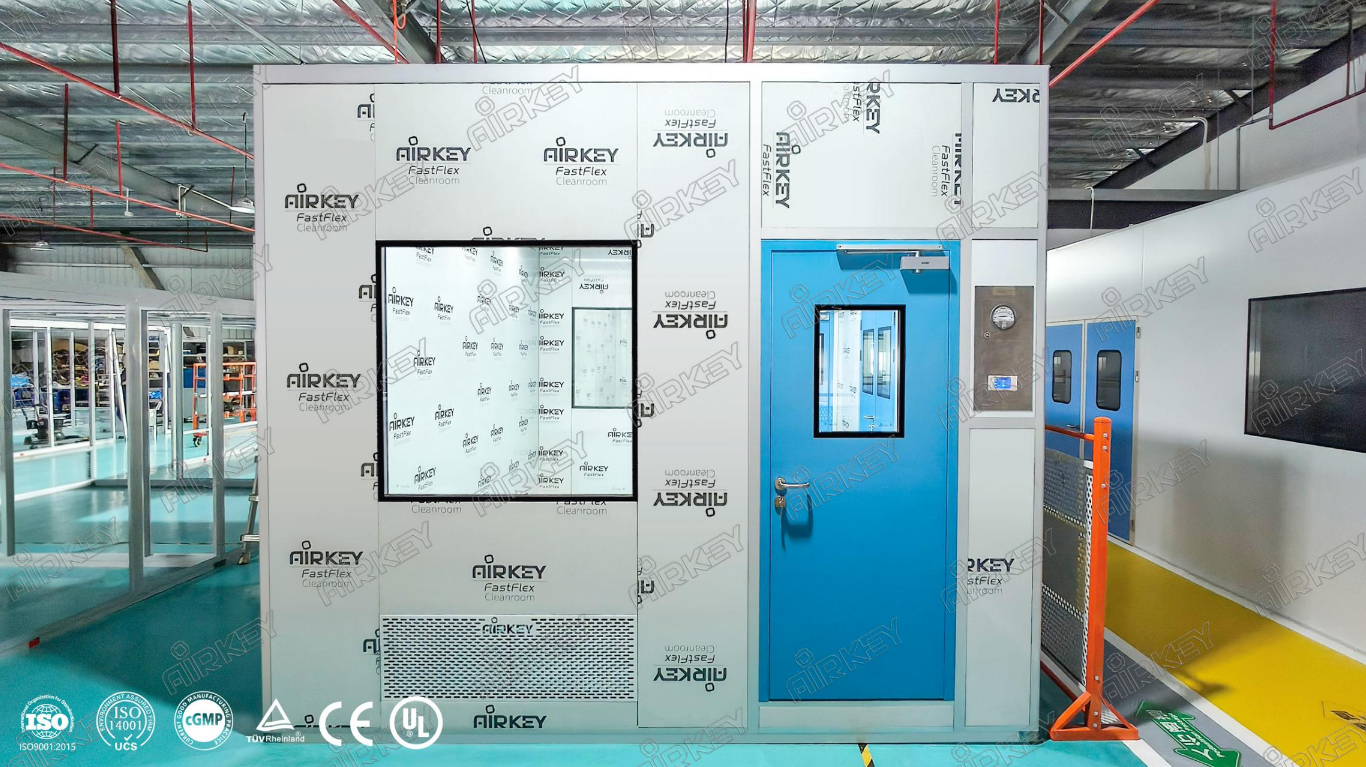
To preserve the existing facility floor while overcoming uneven ground conditions, Airkey implemented an adjustable raised floor system. This solution ensured excellent floor flatness and precise leveling without any modification to the original floor.
Additionally, door heights were customized to align perfectly with the raised floor structure.
The cleanroom was equipped with EC motor FFUs featuring both individual and centralized speed control functions.
Benefits include:
Together with H14 HEPA filters, the system consistently maintains ISO 8 cleanroom standards.
A split-type air conditioning system was installed to maintain stable indoor temperatures and provide a comfortable working environment for laboratory personnel.
All electrical components, including power outlets, are certified to Australian SAA standards, ensuring full compliance with local electrical safety regulations.
Prior to shipment, all cleanroom components underwent comprehensive factory testing.
The customer visited Airkey's manufacturing facility to observe product testing and assembly procedures firsthand.
Critical parameters including:
all passed validation successfully during the first performance test, resulting in high customer satisfaction.
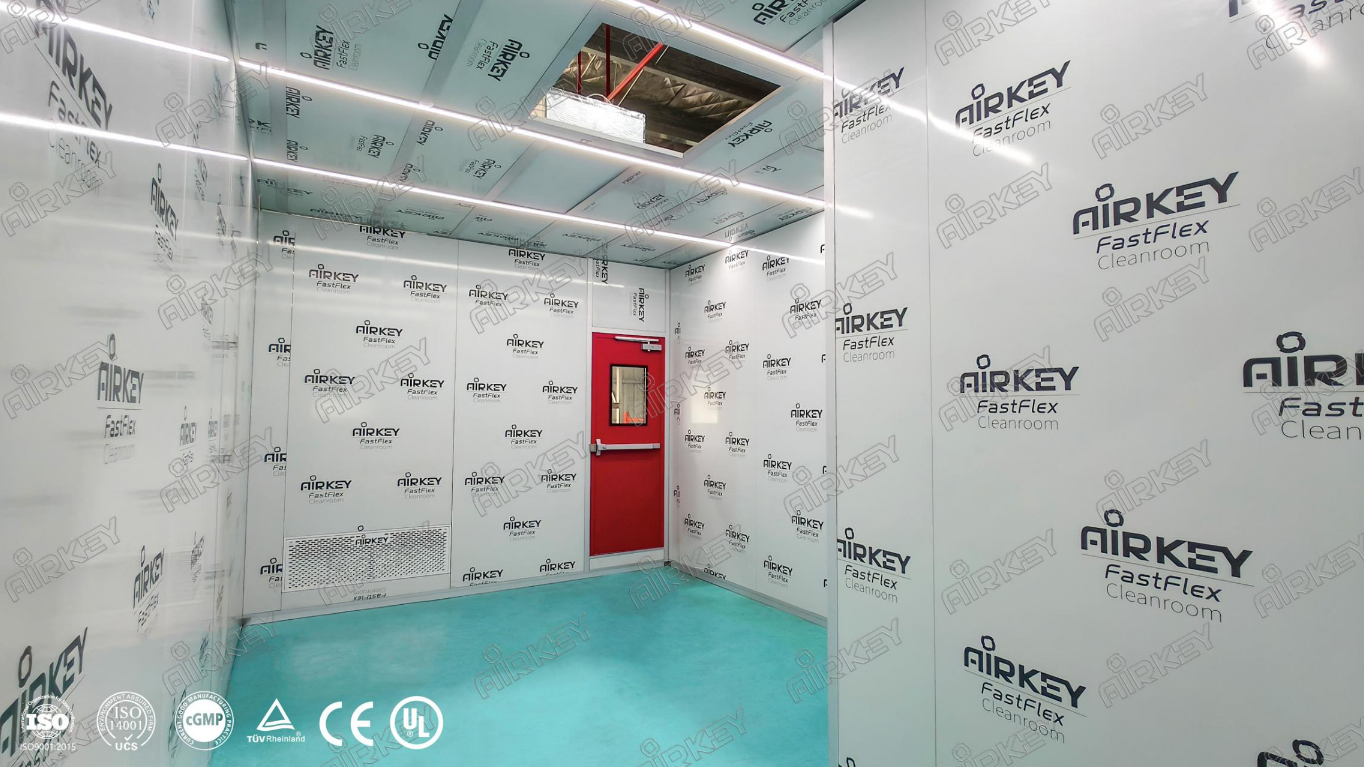
By implementing Airkey's modular cleanroom solution, the client achieved:
ISO 8 cleanroom compliance for pharmaceutical R&D
Faster installation with minimal site disruption
Flexible space for future expansion
Enhanced operational efficiency
Full compliance with Australian safety standards


