


Recent Projects
How Airkey Built an ISO 6 Modular Cleanroom for Neutron Generator Manufacturing
2026-07-06


Aseptic preparation is one of the most contamination-sensitive processes in pharmaceutical and biotechnology manufacturing. From raw material weighing and reagent preparation to sterile processing and final packaging, every production step must be performed in a controlled environment to protect product quality and regulatory compliance.
To meet these requirements, Airkey designed and delivered a customized ISO Class 6 modular cleanroom for a biotechnology company in Texas, USA, creating a GMP-oriented production environment with precise contamination control and efficient workflow management.
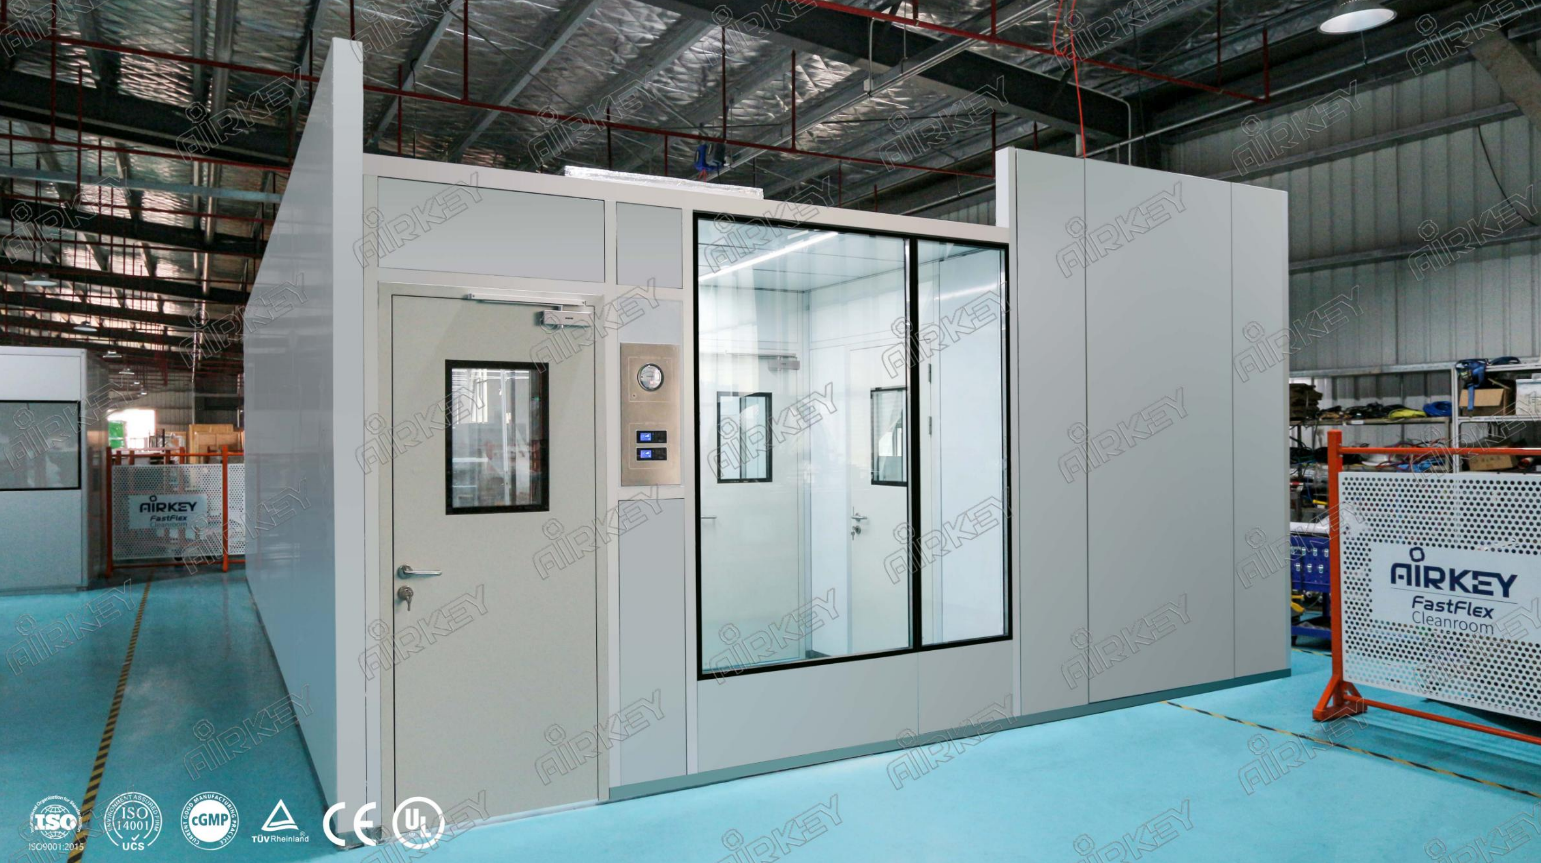
Airkey provided a turnkey modular cleanroom solution for aseptic preparation and life science production.
Designed with prefabricated modular construction, the cleanroom integrates personnel flow, material transfer, environmental monitoring, and contamination control into a single efficient production space.
Location: Texas, USA
Industry: Pharmaceutical
Application: Aseptic Preparation & Biotechnology Production
Cleanliness Level: ISO Class 6 (Class 1000)
Area: 49㎡
Internal Height: 2.5 m
Temperature: 16.8–18.9°C
Humidity: 40–50% RH
Series: Castle Series Modular Cleanroom
The completed cleanroom provides a stable operating environment for biological reagent preparation, sterile processing, quality testing, and packaging.
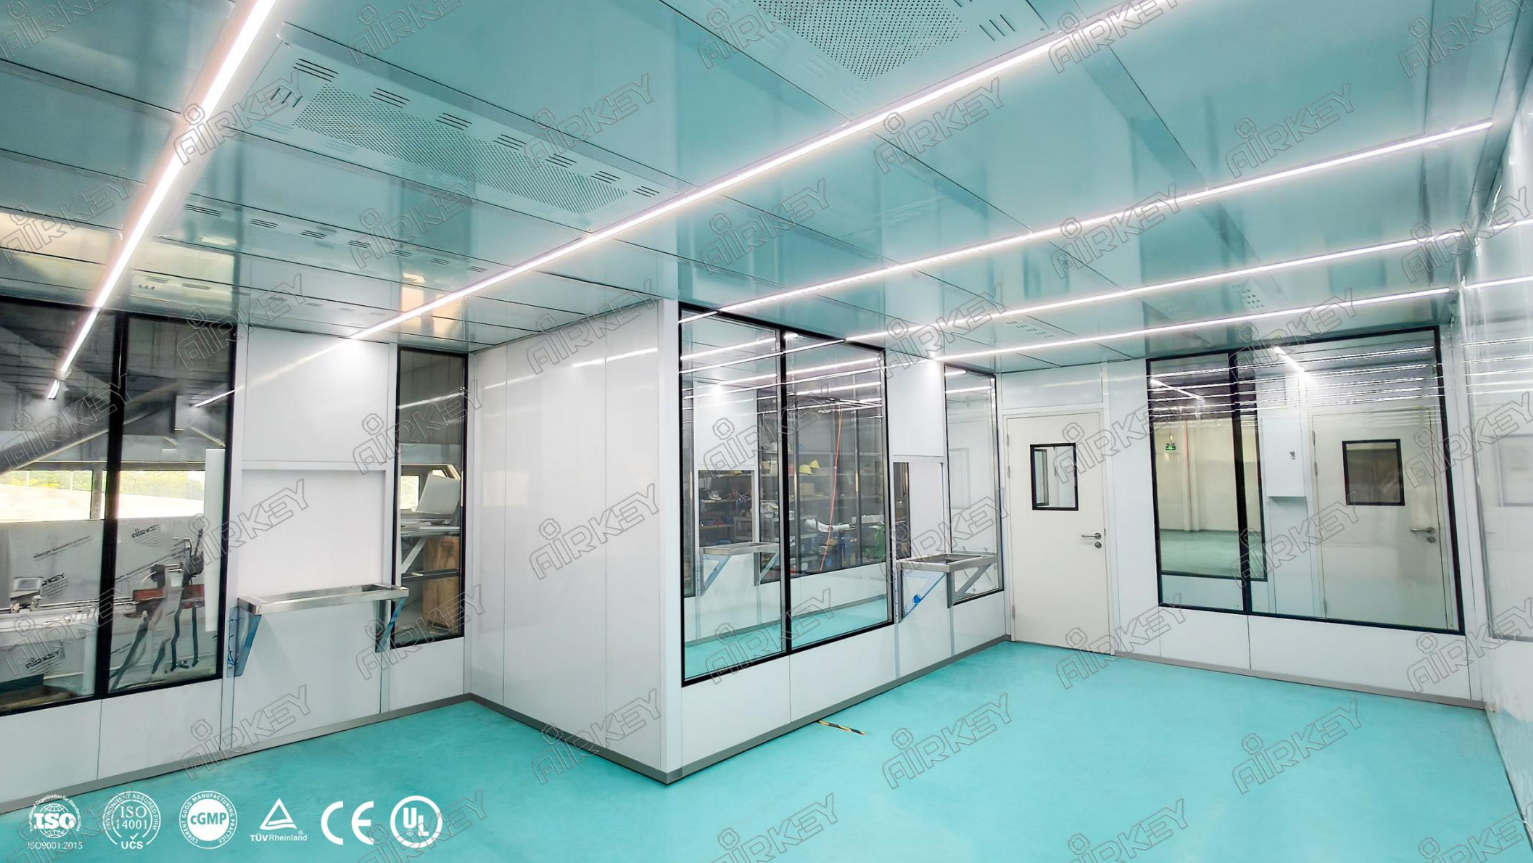
The customer is an innovative biotechnology company located in Texas, USA.
Its manufacturing process includes raw material weighing, reagent preparation, aseptic processing, quality inspection, and final packaging, all of which require strict contamination control and environmental stability throughout production.
Sterile production environments require much more than high cleanliness levels.
Personnel movement, material transfer, room pressure, airflow direction, and temperature and humidity control must all work together to prevent contamination.
Improper workflow design or unstable environmental conditions can increase the risk of cross-contamination, affect product quality, and reduce manufacturing efficiency.
For biotechnology production, integrating functional zoning with controlled airflow is essential to maintaining GMP-compliant operations.
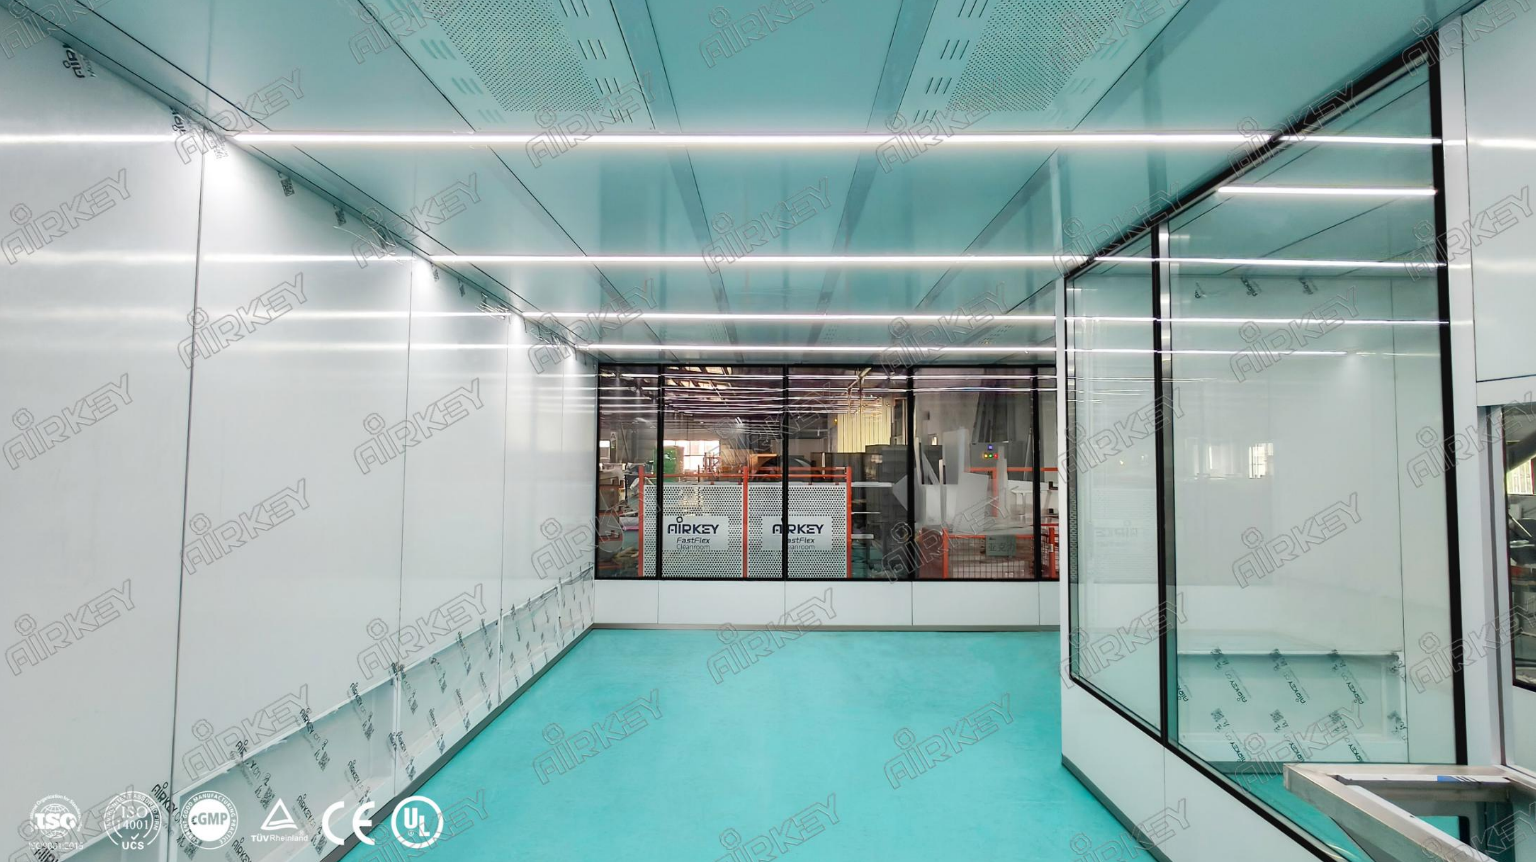
Airkey developed a fully customized modular cleanroom featuring a self-supporting aluminum structure with prefabricated wall panels for rapid installation and future expansion.
Large double-glazed observation windows provide excellent visibility, allowing supervisors to monitor production activities without entering the cleanroom.
The system integrates differential pressure monitoring and environmental controls to maintain stable operating conditions.
An innovative return air wall design eliminates traditional return air columns, maximizing usable floor space while improving cleanability and maintenance efficiency.
To support biotechnology production, the cleanroom also incorporates biosafety cabinets, pass-through chambers, dedicated gowning areas, and logical personnel and material flow to reduce contamination risks and support GMP compliance.
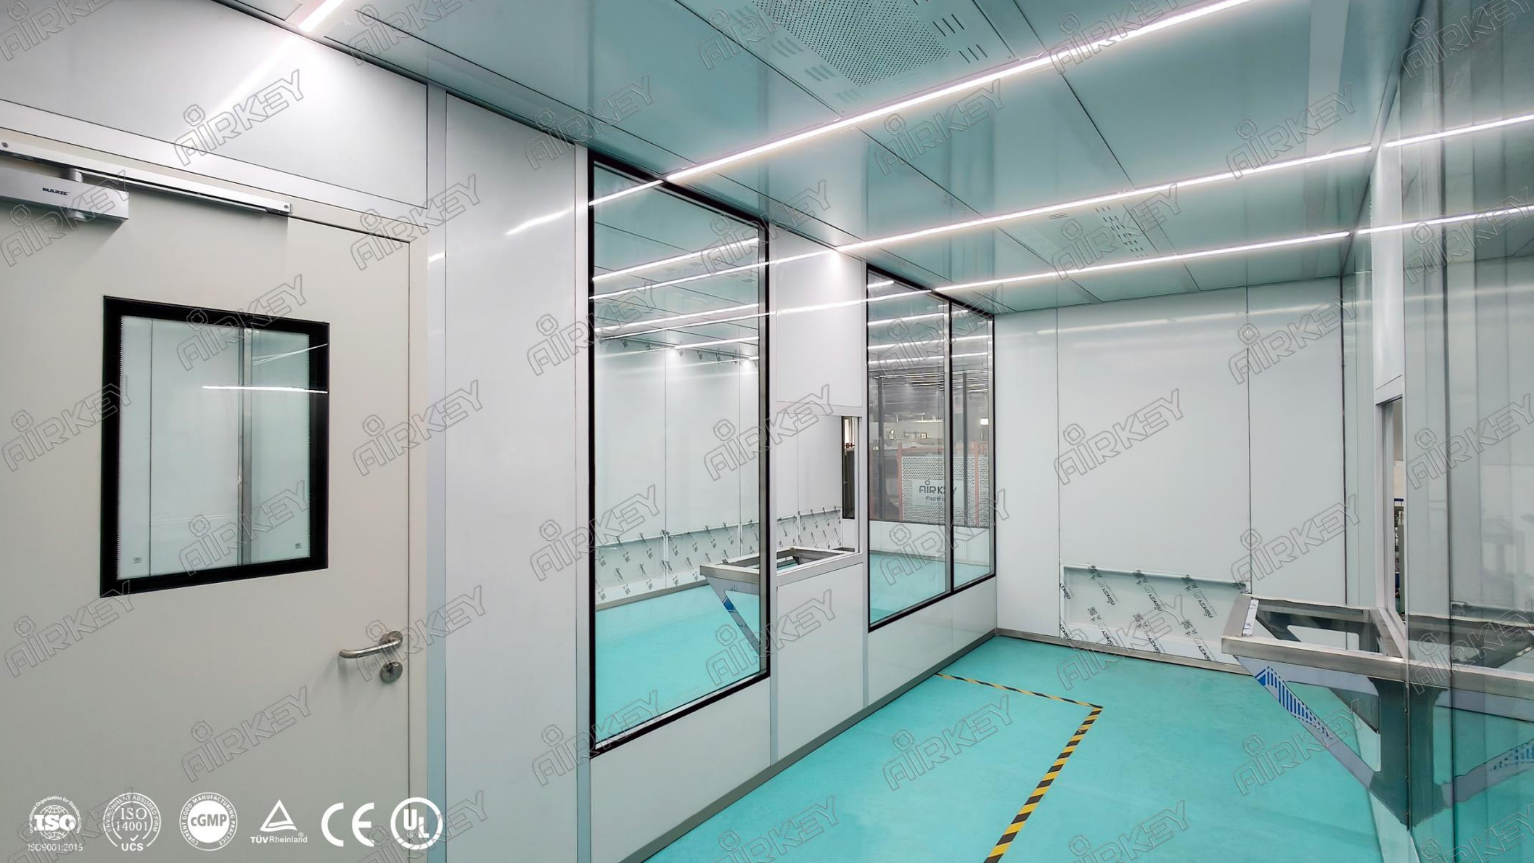
Compared with conventional cleanroom construction, Airkey's modular cleanroom enables faster installation, flexible expansion, and simplified maintenance.
Its integrated return air system and intelligent environmental monitoring improve airflow distribution while maintaining stable cleanliness, temperature, and humidity.
The modular design also reduces construction downtime, making it an ideal solution for rapidly expanding pharmaceutical and biotechnology facilities.
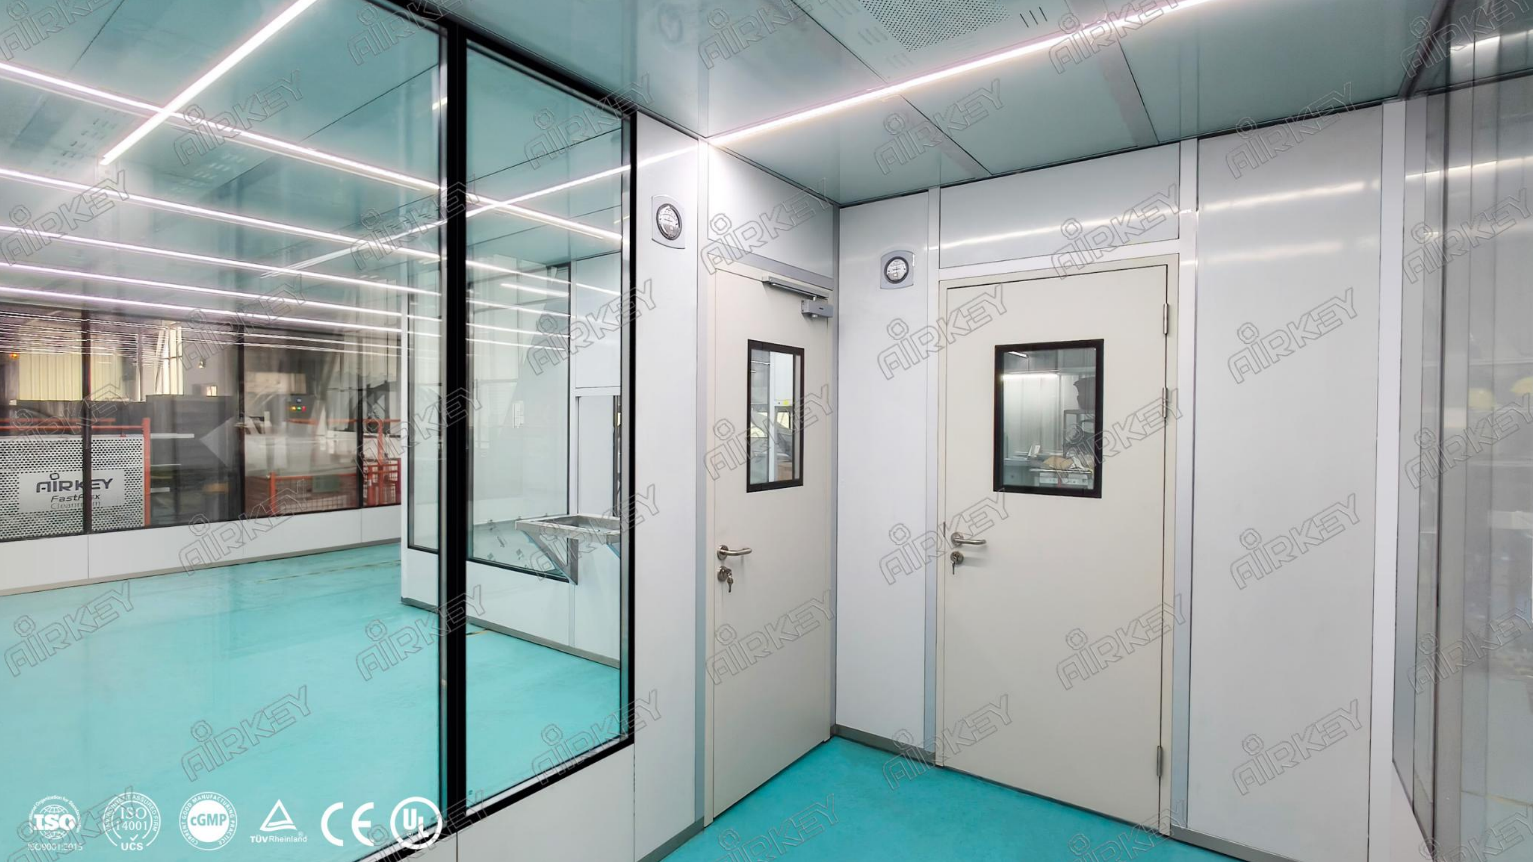
ISO Class 6 provides controlled airborne particle levels suitable for sterile preparation, reagent handling, and other pharmaceutical manufacturing processes requiring contamination control.
Yes. The layout incorporates personnel and material segregation, pressure cascades, contamination control measures, and functional zoning designed to support GMP-compliant production.
Yes. The prefabricated modular structure allows future modifications and expansion with minimal disruption.
Yes. Airkey provides complete services including cleanroom design, manufacturing, HVAC integration, installation, validation, and after-sales support worldwide.
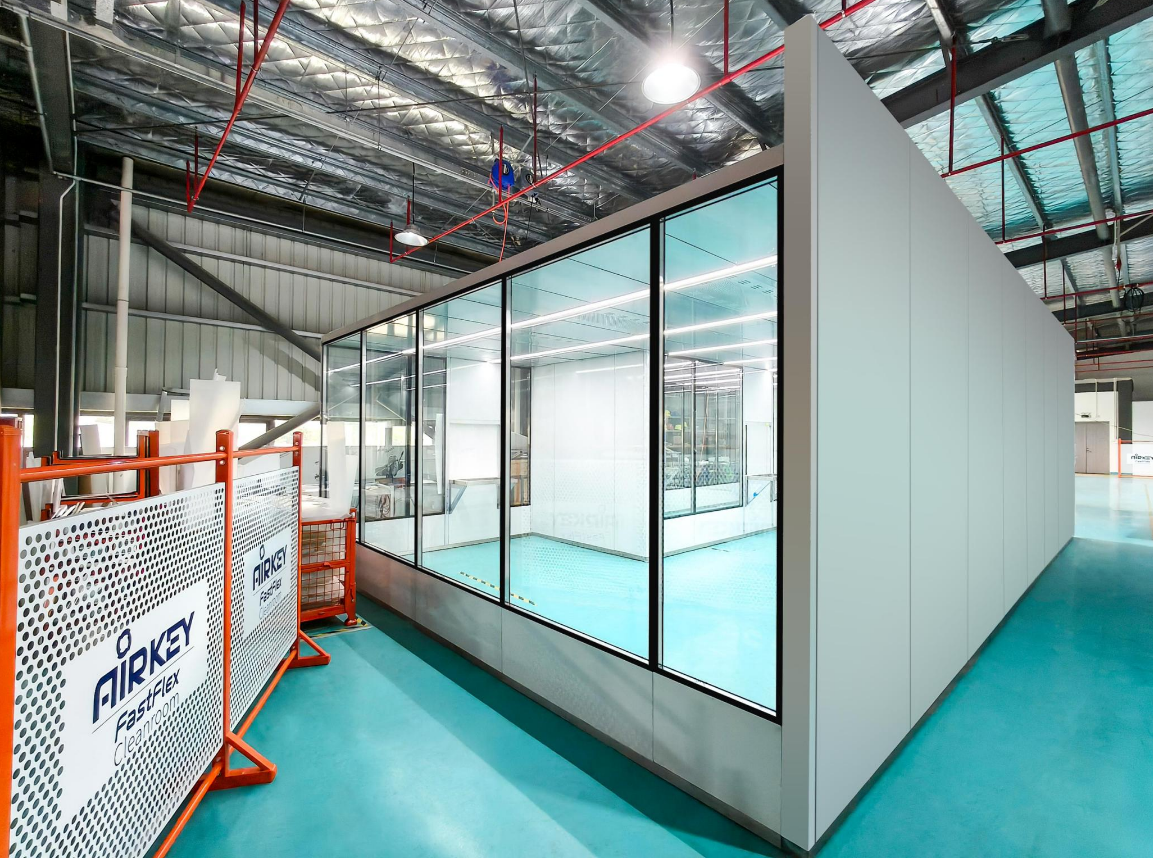
The completed ISO Class 6 modular cleanroom now provides a stable, contamination-controlled environment for aseptic preparation and biotechnology manufacturing.
By combining modular construction, intelligent environmental monitoring, and optimized workflow design, the project helps the customer improve operational efficiency while maintaining ISO 14644 and GMP-compliant production standards.
Airkey specializes in modular cleanroom solutions for pharmaceutical manufacturing, biotechnology, medical devices, laboratories, and other contamination-sensitive industries.
Whether you require ISO Class 5, ISO Class 6, or GMP-compliant cleanrooms, our engineering team delivers complete turnkey solutions from design and fabrication to installation and validation.


