


Recent Projects
Laser Machinery Manufacturing -Modular Cleanroom
2026-06-04


Airkey successfully completed the design and manufacturing of a 55㎡ ISO 8 modular cleanroom for a pharmaceutical company located in Colorado, USA. The project was developed to support solid dosage production processes including granulation, blending, tablet compression, and packaging, while meeting strict environmental control requirements for pharmaceutical manufacturing.
The customer specializes in developing and producing high-performance pharmaceutical formulations. As production capacity expanded, the company required a cleanroom solution capable of maintaining stable cleanliness, temperature, and humidity conditions while minimizing cross-contamination risks throughout the manufacturing process.
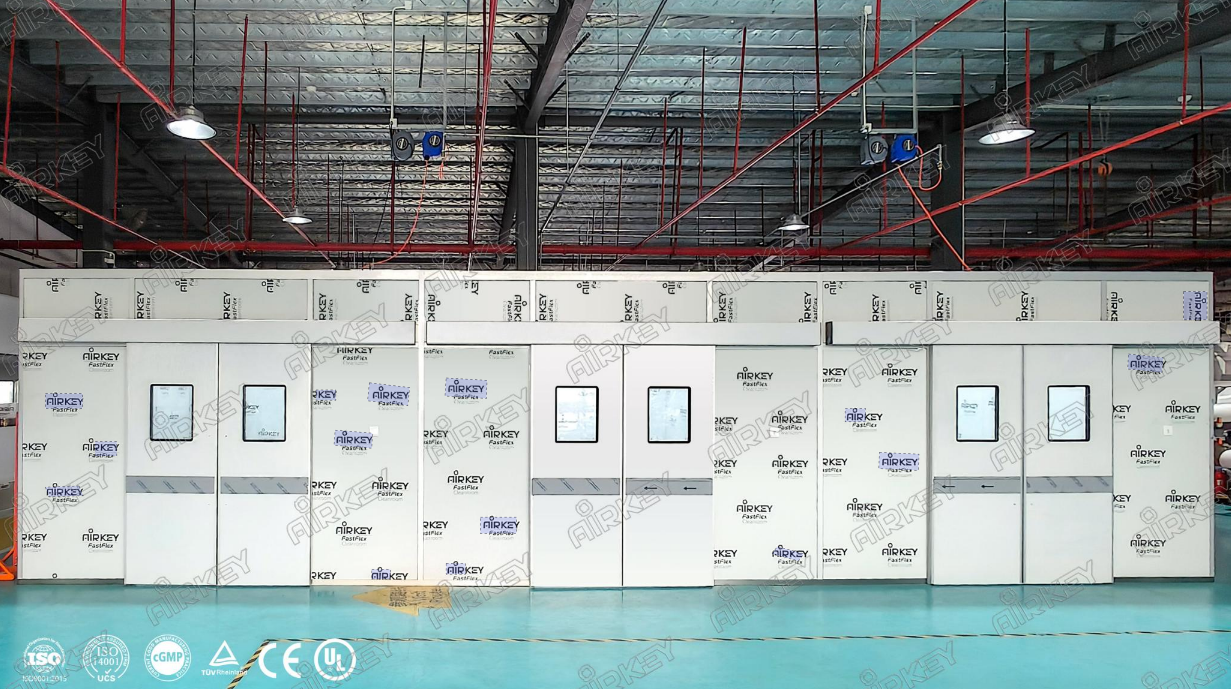
| Item | Details |
|---|---|
| Project Name | Solid Dosage ISO 8 Modular Cleanroom |
| Industry | Pharmaceutical |
| Location | Colorado, USA |
| Cleanliness Level | ISO 8 (Class 100,000) |
| Area | 55㎡ |
| Internal Height | 2.7 m |
| Temperature | 20–24°C |
| Relative Humidity | 45–50% RH |
Solid dosage manufacturing involves multiple critical processing stages, including powder handling, granulation, blending, tablet compression, and final packaging. Each stage generates different levels of airborne particles and dust, creating significant challenges for contamination control.
To ensure product consistency and GMP compliance, the client required a cleanroom environment that could:
Airkey designed a modular cleanroom solution tailored specifically to these operational requirements.
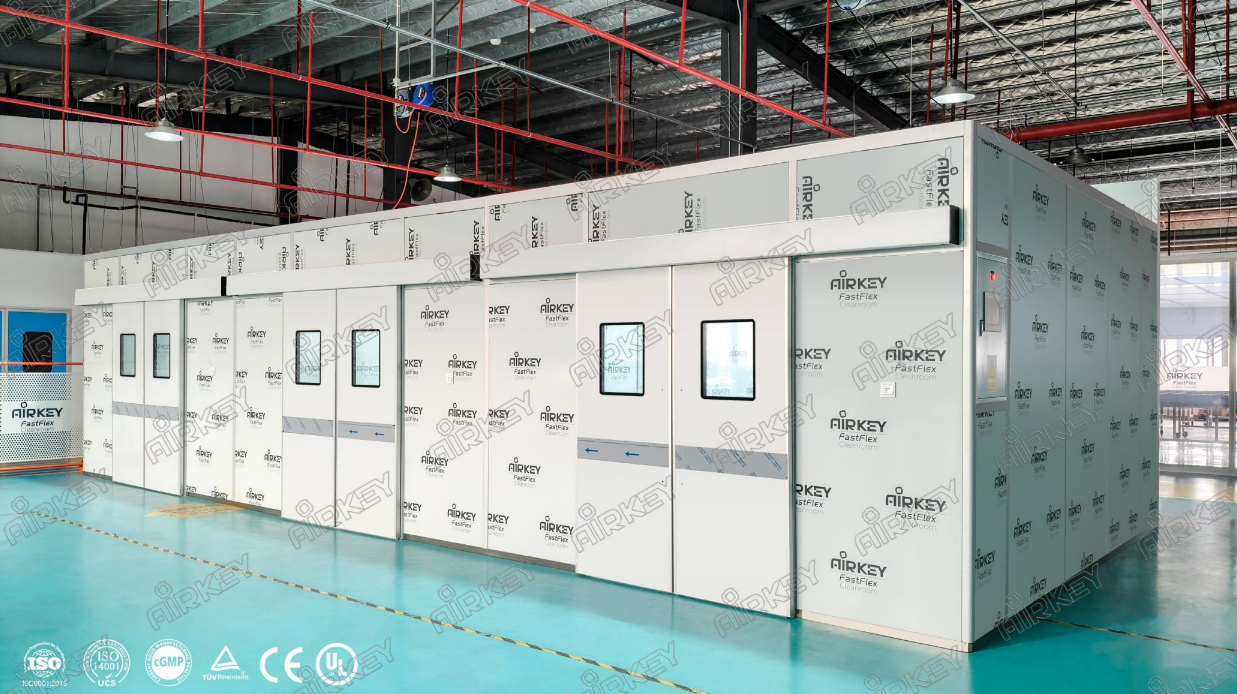
The cleanroom was designed as a complete room-within-a-room system that integrates the entire production workflow within a controlled environment.
The self-supporting aluminum structure eliminates the need for ceiling suspension or wall anchoring, making it ideal for leased facilities where structural modifications are restricted. This design also provides greater flexibility for future expansion or relocation.
High-quality rock wool sandwich panels were selected to create a GMP-compliant enclosure with excellent fire resistance, airtightness, and cleanability. The smooth surfaces help reduce particle accumulation and simplify routine cleaning procedures.
To improve operational efficiency, the cleanroom incorporates automatic sliding doors that facilitate material transfer while minimizing airflow disturbance. Double-glazed observation windows allow operators and supervisors to monitor production activities without entering critical process areas.
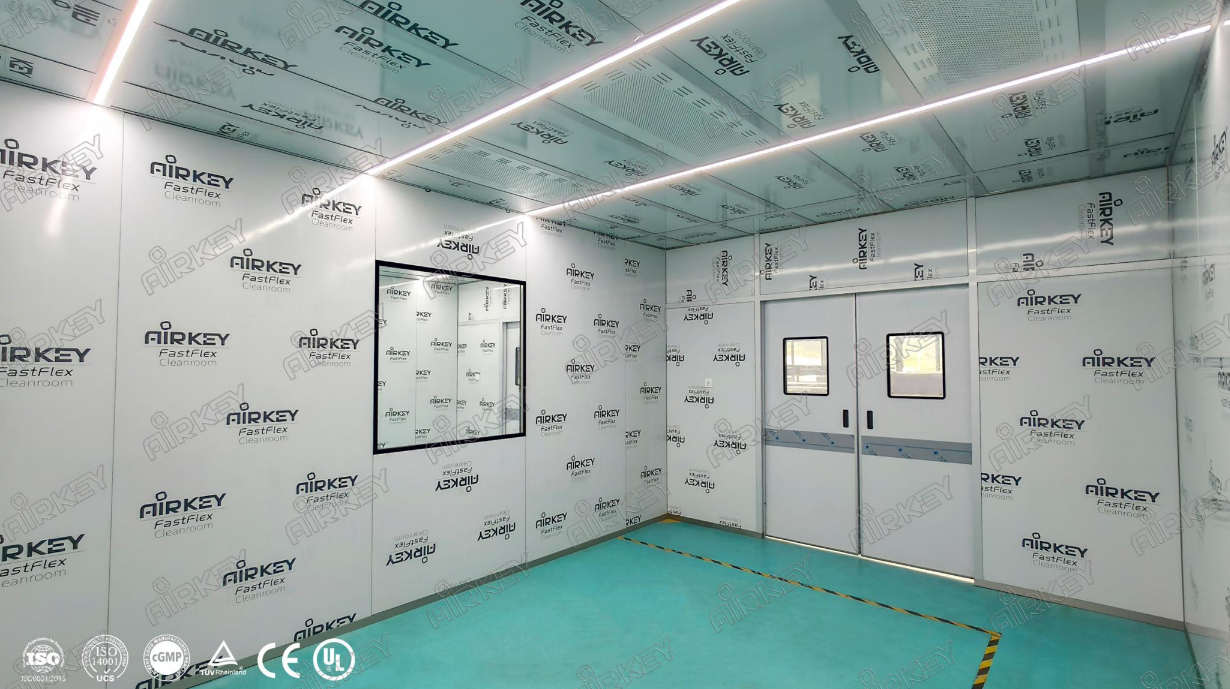
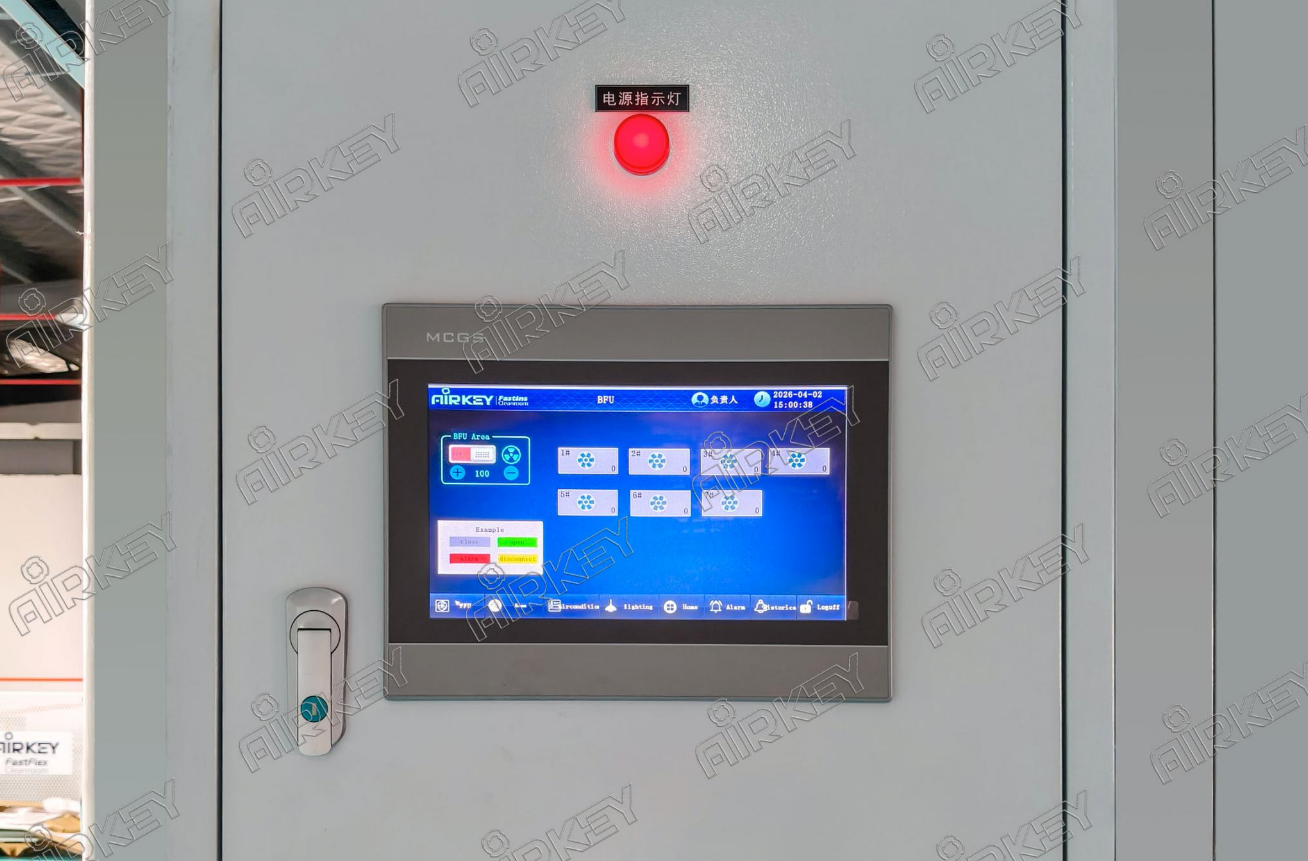
A centralized monitoring system continuously tracks temperature, humidity, and differential pressure throughout the cleanroom.
The system also enables precise control of FFUs, ensuring stable airflow and consistent ISO 8 cleanliness performance.
One of the key technical features of this project is Airkey’s patented return air wall panel system. Unlike traditional ducted return air designs, the 100 mm integrated return air panels improve space utilization while promoting uniform airflow distribution throughout the cleanroom.
This innovative design helps eliminate airflow dead zones and contributes to stable environmental conditions across all production areas.
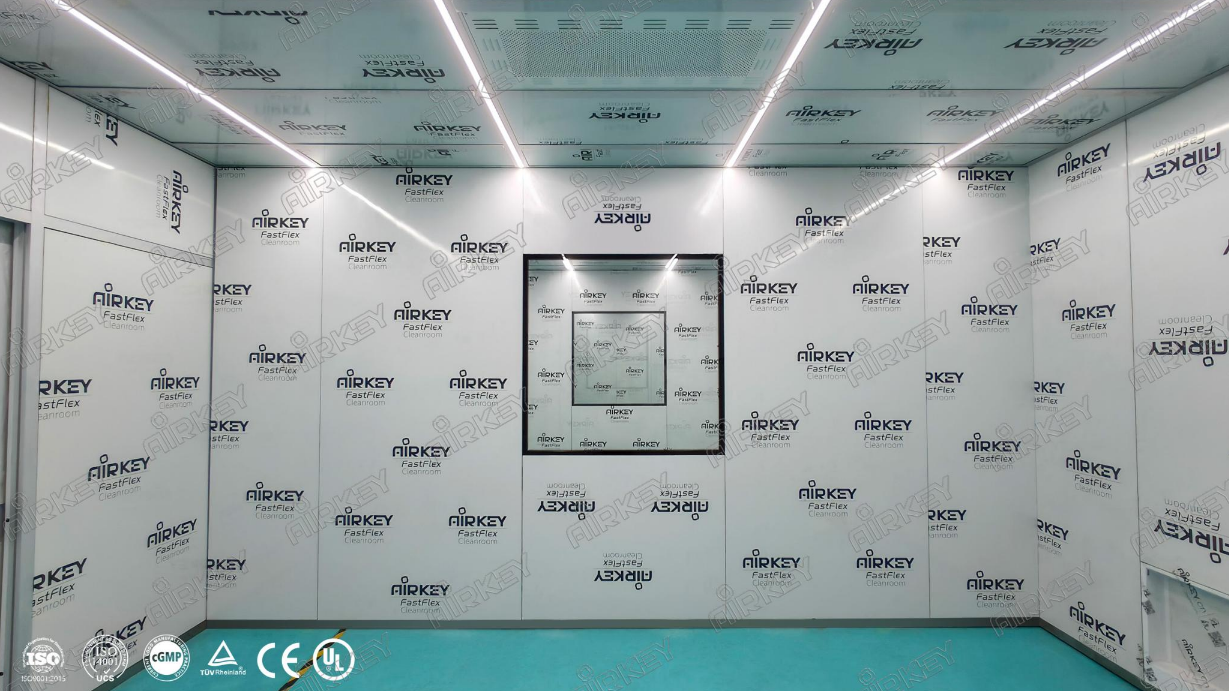
The cleanroom utilizes a fully independent aluminum frame system, making installation faster and more flexible without requiring modifications to the building structure.
Rock wool sandwich panels provide excellent airtightness, fire resistance, and contamination control performance.
Automatic sliding doors and observation windows improve workflow efficiency while reducing contamination risks.
Integrated monitoring and control systems ensure stable temperature, humidity, pressure, and cleanliness levels.
Airkey's patented return air panel system enhances airflow uniformity and maximizes usable interior space.
All electrical components comply with North American standards, enabling efficient installation and commissioning on site.
The completed ISO 8 modular cleanroom provides a stable, compliant, and highly efficient production environment for pharmaceutical solid dosage manufacturing. By combining modular construction with advanced environmental control technology, Airkey delivered a solution that supports regulatory compliance, operational efficiency, and future production growth.
The project demonstrates Airkey's capability to provide customized modular cleanroom solutions for pharmaceutical manufacturers worldwide, helping customers achieve reliable environmental control while reducing installation time and operational complexity.


