


Recent Projects
ISO 5 Modular Cleanroom Solution for Peptide Production in the USA
2026-08-10

Peptide production requires a highly controlled manufacturing environment because particulate and microbial contamination can affect synthesis yield, purification efficiency, product quality, and final release testing.
For a GMP-oriented peptide production facility in the USA, Airkey designed and delivered a 23㎡ ISO Class 5 modular cleanroom using the Light Series. The solution combines a stable ISO 5 environment, personnel decontamination, high-efficiency EC FFUs, professional lighting, and factory-prefabricated construction to support contamination-sensitive peptide production processes.
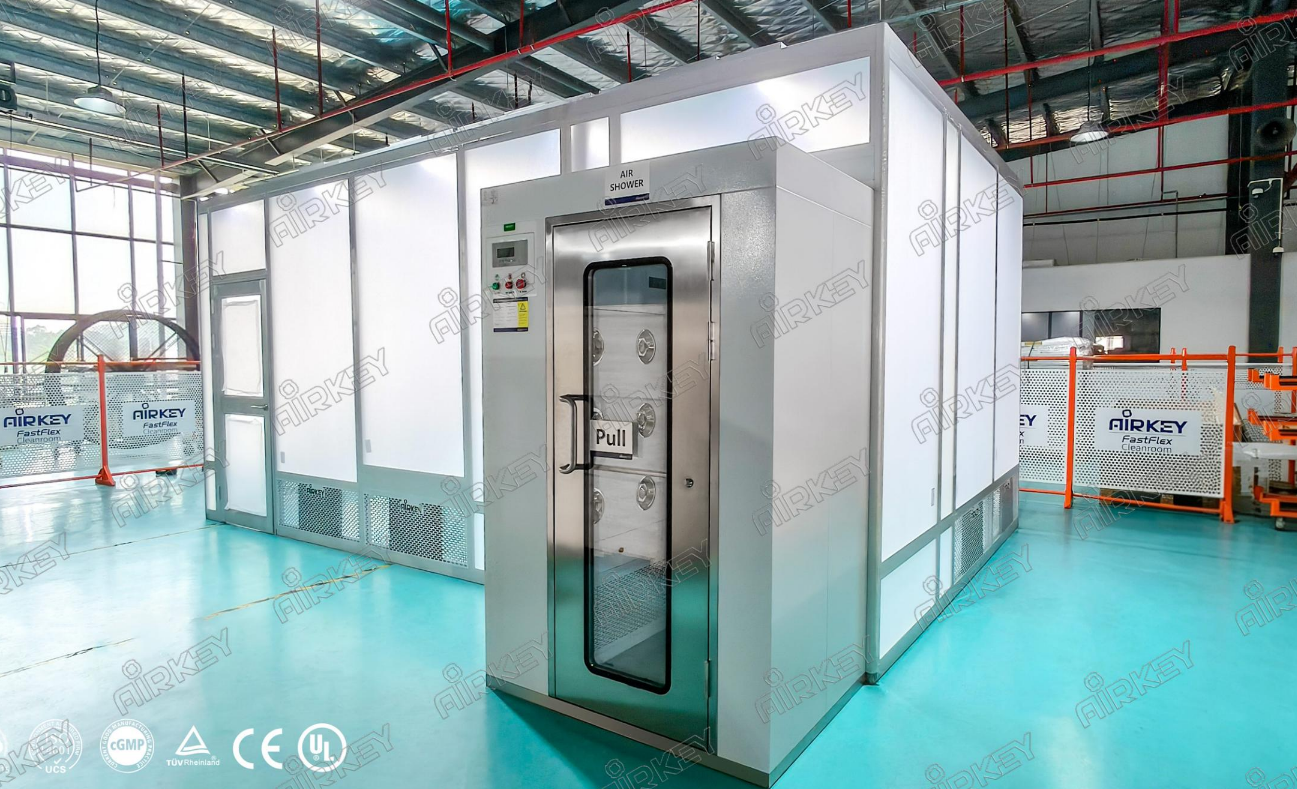
| Item | Specification |
|---|---|
| Project | ISO 5 Peptide Production Modular Cleanroom |
| Location | USA |
| Industry | Peptide Production |
| Cleanliness | ISO Class 5 |
| Area | 23㎡ |
| Internal Height | 2.75 m |
| Series | Light Series |
| Model | FAG-I5N-A23(6.1 × 3.66 × 3.05)-F |
The customer is a US-based peptide production company operating in the biopharmaceutical field and focused on customized peptides and APIs under GMP-oriented production conditions.
Peptide manufacturing involves several contamination-sensitive stages.
Impurities and airborne particles can contribute to peptide chain degradation, potentially reducing synthesis yield and affecting the purity and quality of the final product.
Environmental particles may affect chromatography processes and reduce purification efficiency, potentially impacting final product purity.
Microorganisms or foreign matter entering inner packaging materials can create contamination risks, including excessive endotoxins or visible foreign matter in the final product.
Analytical processes such as HPLC and microbial limit testing require a controlled environment to minimize environmental interference and support reliable quality-control results.
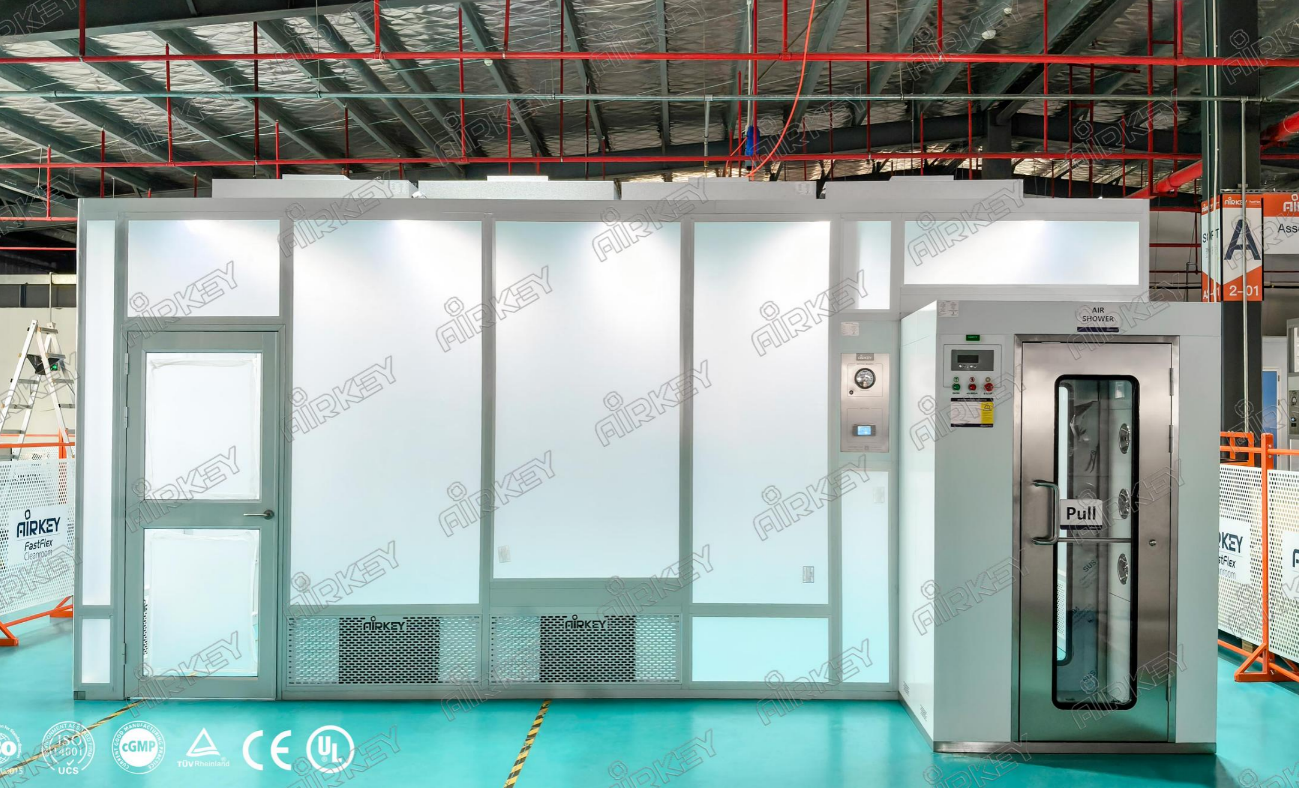
Airkey selected its Light Series modular cleanroom to create a bright, clean, and visually open production environment.
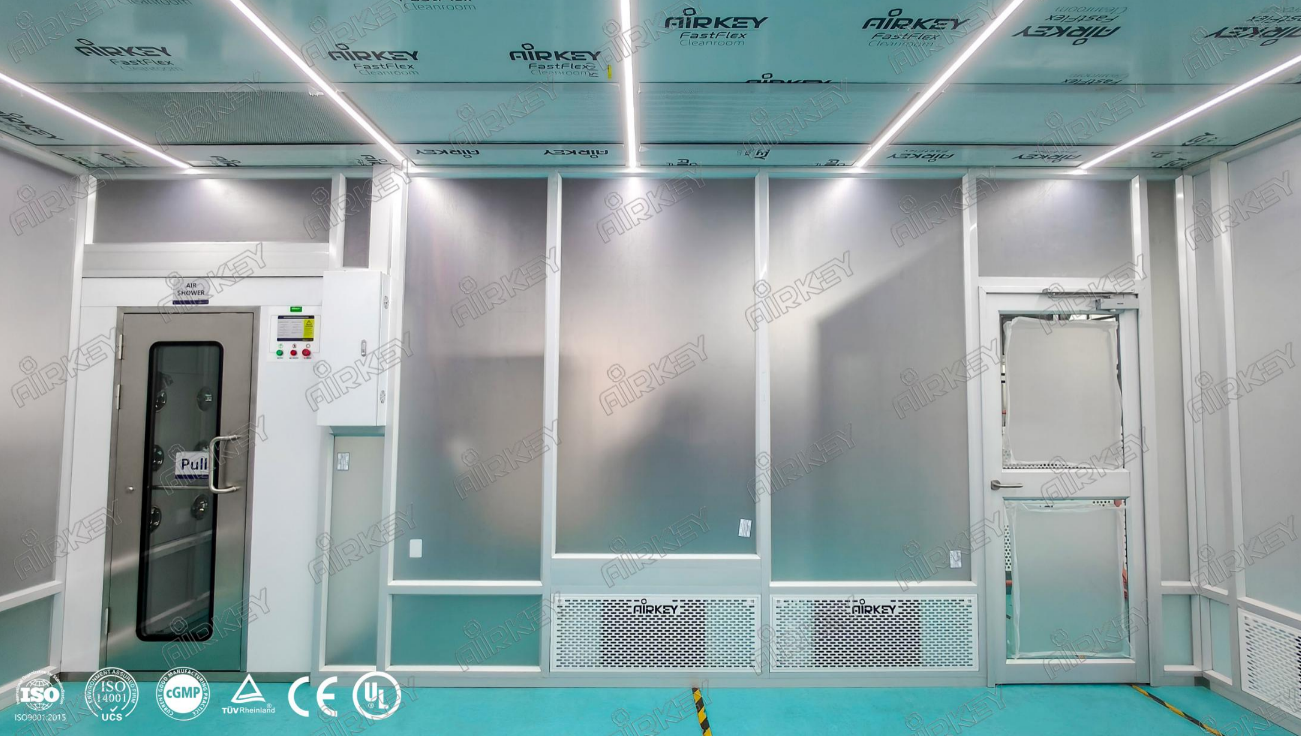
The structure combines an aluminum frame with acrylic wall panels, providing high visibility while maintaining a simple and modern appearance. The dust-resistant, screwless design also reduces potential particle-generation points inside the cleanroom.
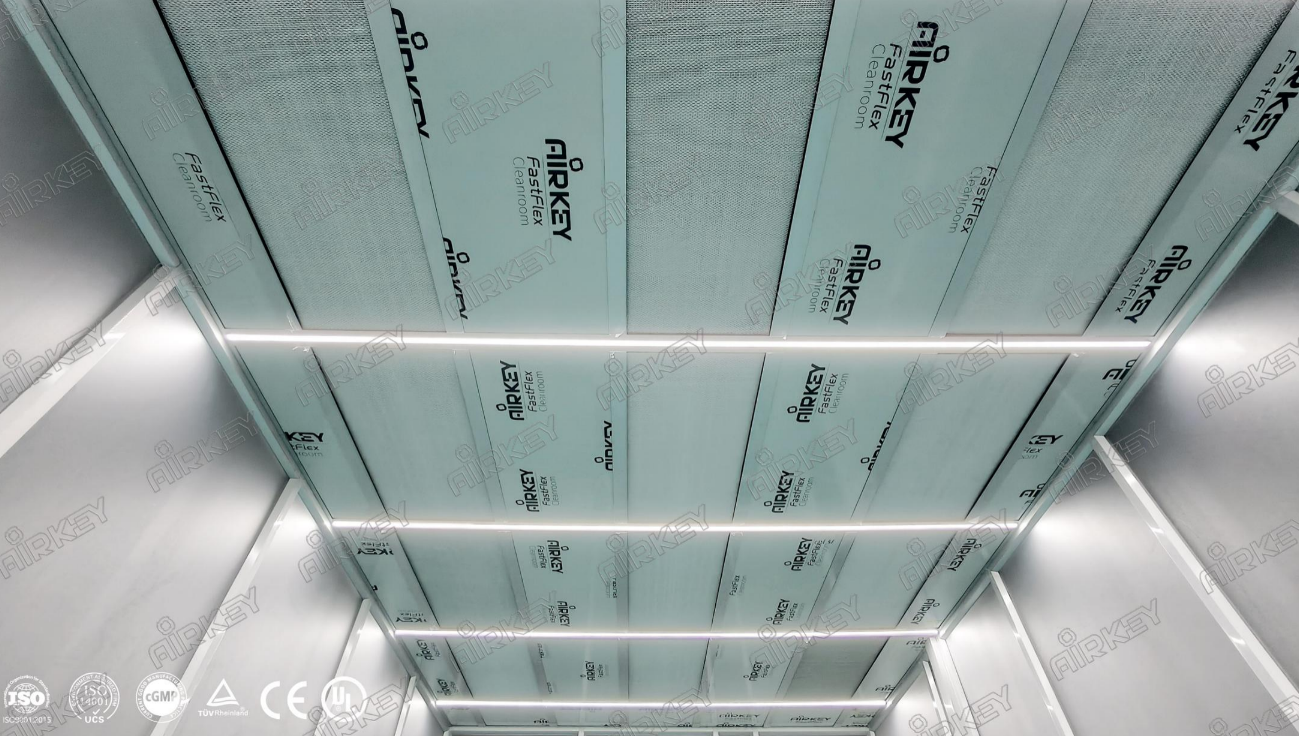
The cleanroom is equipped with 12 top-mounted EC FFUs designed to provide high airflow with low noise and low energy consumption.
The FFU system helps maintain ISO Class 5 cleanliness across the working area, while the control panel allows the operator to adjust airflow speed and lighting according to operational requirements.
An integrated air shower removes surface dust from personnel before they enter the cleanroom.
The interlocking system also separates clean and non-clean zones, helping maintain stable pressure and reduce contamination ingress during personnel movement.
High-illuminance LED line lights are flush-mounted into the ceiling.
The smooth, dust-resistant surface helps preserve airflow organization while providing sufficient illumination for peptide production operations, supporting both visibility and cleanroom hygiene requirements.
The modular cleanroom was fully prefabricated and tested at Airkey's factory before shipment.
Cleanroom parameters including cleanliness, temperature, and illuminance were tested before delivery, allowing the system to be rapidly deployed and used after on-site power connection.
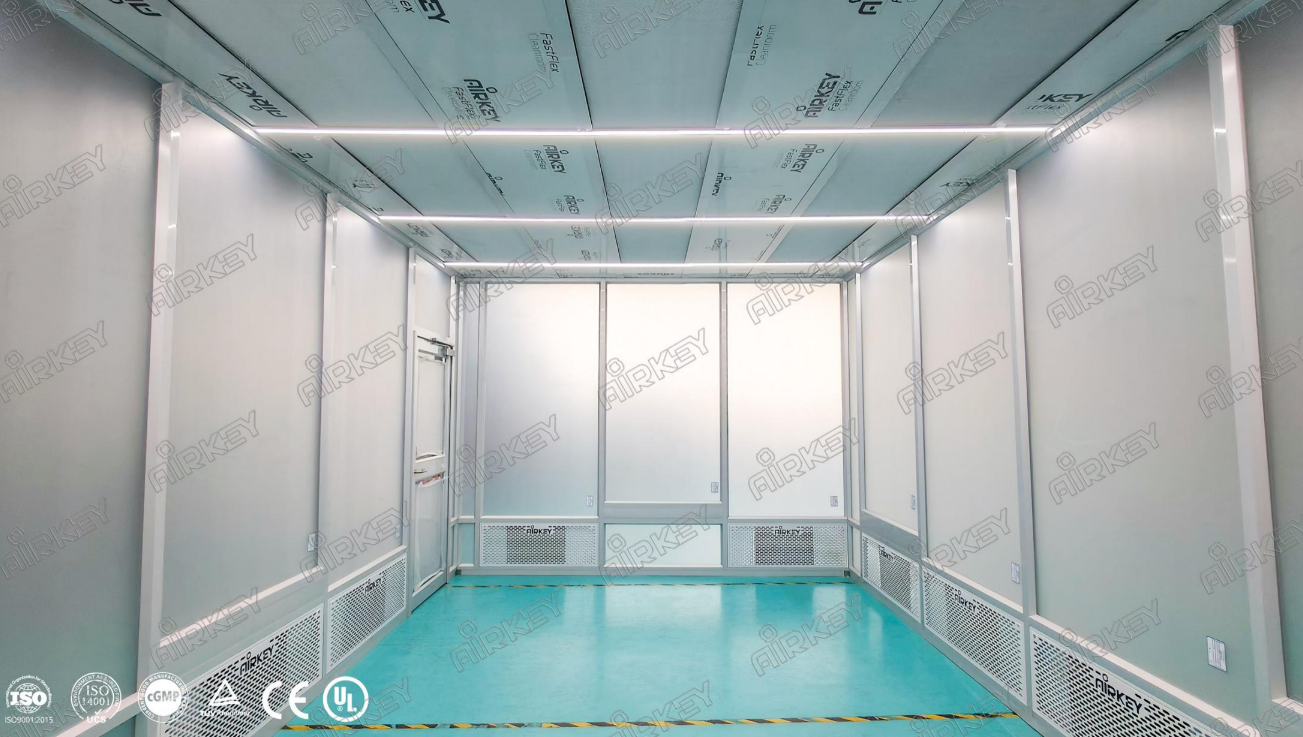
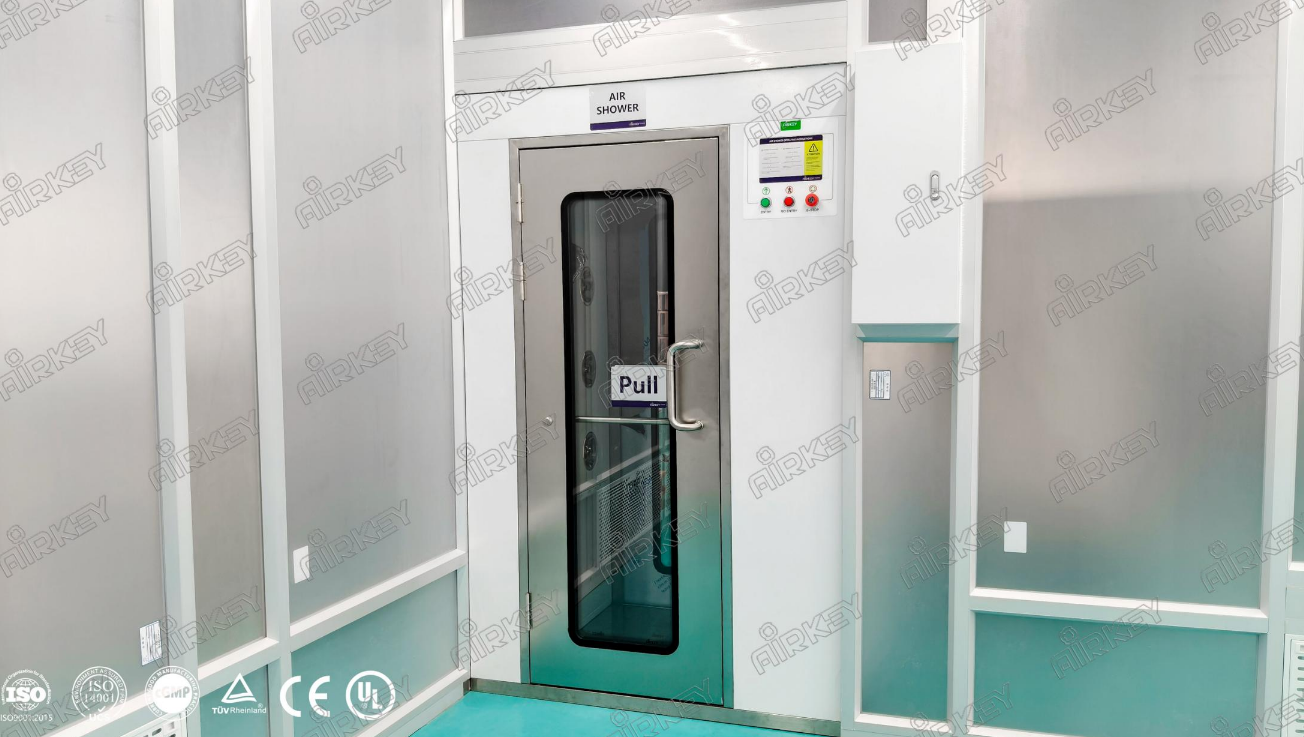
The completed ISO 5 modular cleanroom provides a stable and controllable environment for peptide production in the USA.
By combining high-efficiency EC FFUs, personnel decontamination, controlled entry, professional lighting, and factory testing, the solution addresses the contamination-control requirements associated with peptide manufacturing while providing a bright and efficient production workspace.
The project uses an ISO Class 5 modular cleanroom with a total area of 23㎡.
Contamination can affect peptide synthesis, purification, aseptic filling, and quality-control processes. The project documentation specifically identifies risks associated with particles, microorganisms, and foreign matter throughout these stages.
The cleanroom uses 12 top-mounted EC FFUs to provide high airflow and maintain ISO 5 cleanliness throughout the working area.
An air shower removes surface dust from personnel, while an interlocking system separates clean and non-clean zones to help maintain stable pressure and prevent contamination ingress.
Yes. The modular cleanroom was prefabricated and tested at Airkey's factory, including cleanliness, temperature, and illuminance parameters.
Airkey designs and manufactures modular cleanrooms for peptide production, pharmaceutical manufacturing, biotechnology, APIs, laboratories, and other contamination-sensitive applications.
Our factory-prefabricated modular systems can be customized according to cleanliness classification, production process, layout, airflow requirements, and site conditions.


