Tanzania Biological Reagent Packaging Modular Cleanroom Project Overview
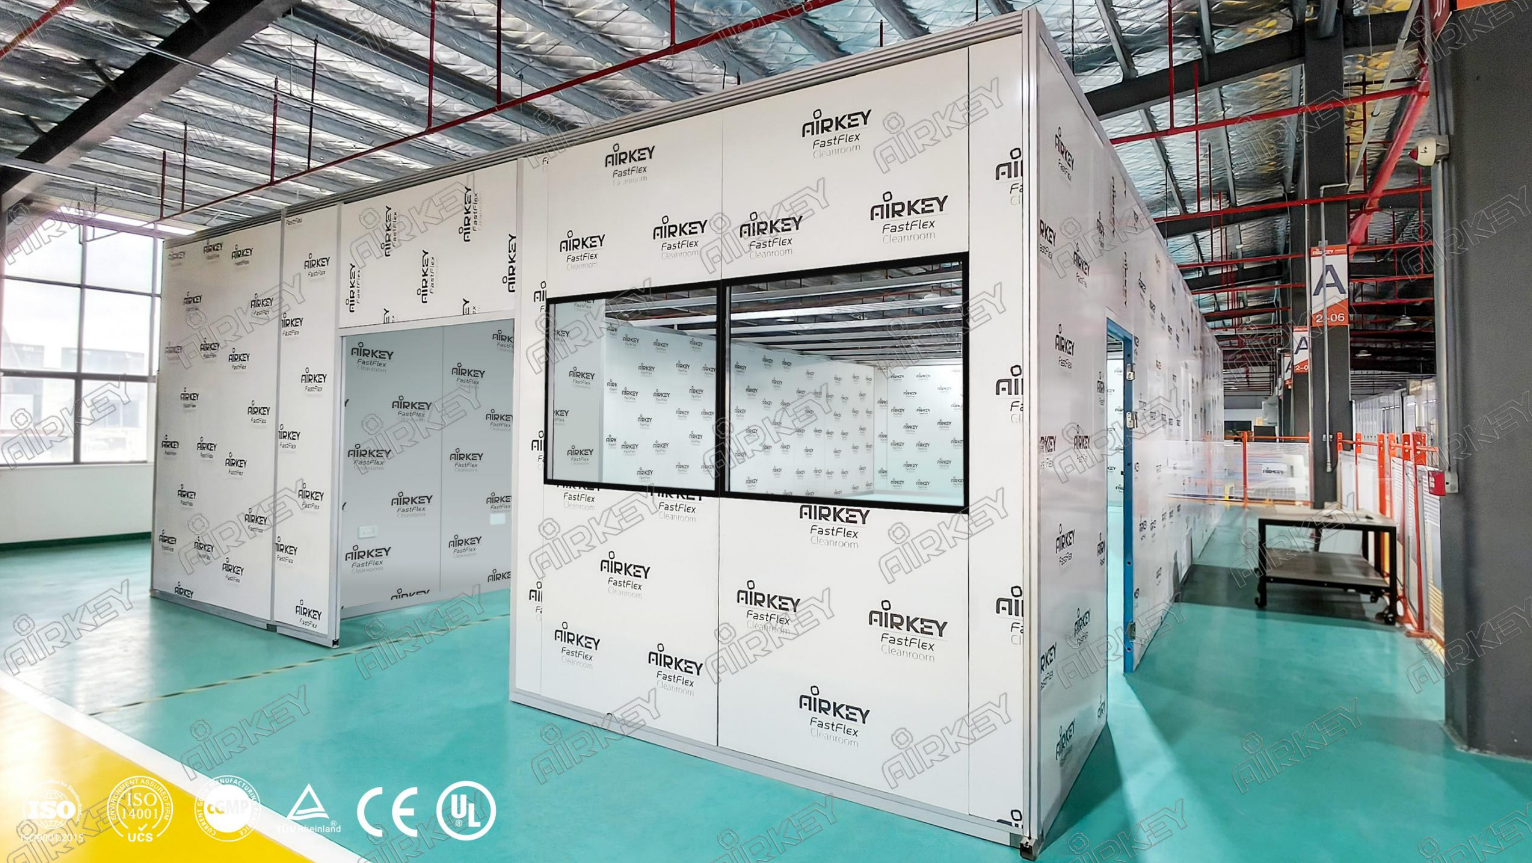
AIRKEY designed and delivered a 391㎡ modular cleanroom for a leading biotechnology company in Dar es Salaam, Tanzania. Developed for biological reagent packaging and diagnostic reagent manufacturing, the project provides a stable and contamination-controlled production environment that complies with international cleanroom standards while supporting efficient local manufacturing.
Built to ISO 9 cleanliness standards, the modular cleanroom incorporates intelligent environmental control, flexible production zoning, and rapid modular installation. The project enables the client to expand production capacity while maintaining consistent product quality and regulatory compliance.
Client Background
LifeDX Africa Co., Limited is a biotechnology company dedicated to improving diagnostic capabilities across Sub-Saharan Africa. The company provides comprehensive research, development, and manufacturing solutions for rapid diagnostic products while supporting technology transfer and localized medical manufacturing.
Its product portfolio includes rapid diagnostic test kits, next-generation sequencing (NGS) solutions, ELISA diagnostic systems, and veterinary diagnostic products. These applications require highly controlled manufacturing environments that ensure product consistency, contamination control, and compliance with international quality standards.
Modular Cleanroom Designed for Biological Reagent Manufacturing
Biological reagent production requires a manufacturing environment that combines cleanliness, flexibility, and regulatory compliance. AIRKEY's modular cleanroom solution was specifically designed to meet these demanding production requirements.
The cleanroom complies with ISO 14644 and GMP standards, providing clean environments ranging from GMP Grade A to Grade D to accommodate different production processes. This standardized design supports both domestic manufacturing and international export requirements while facilitating future technology transfer projects.
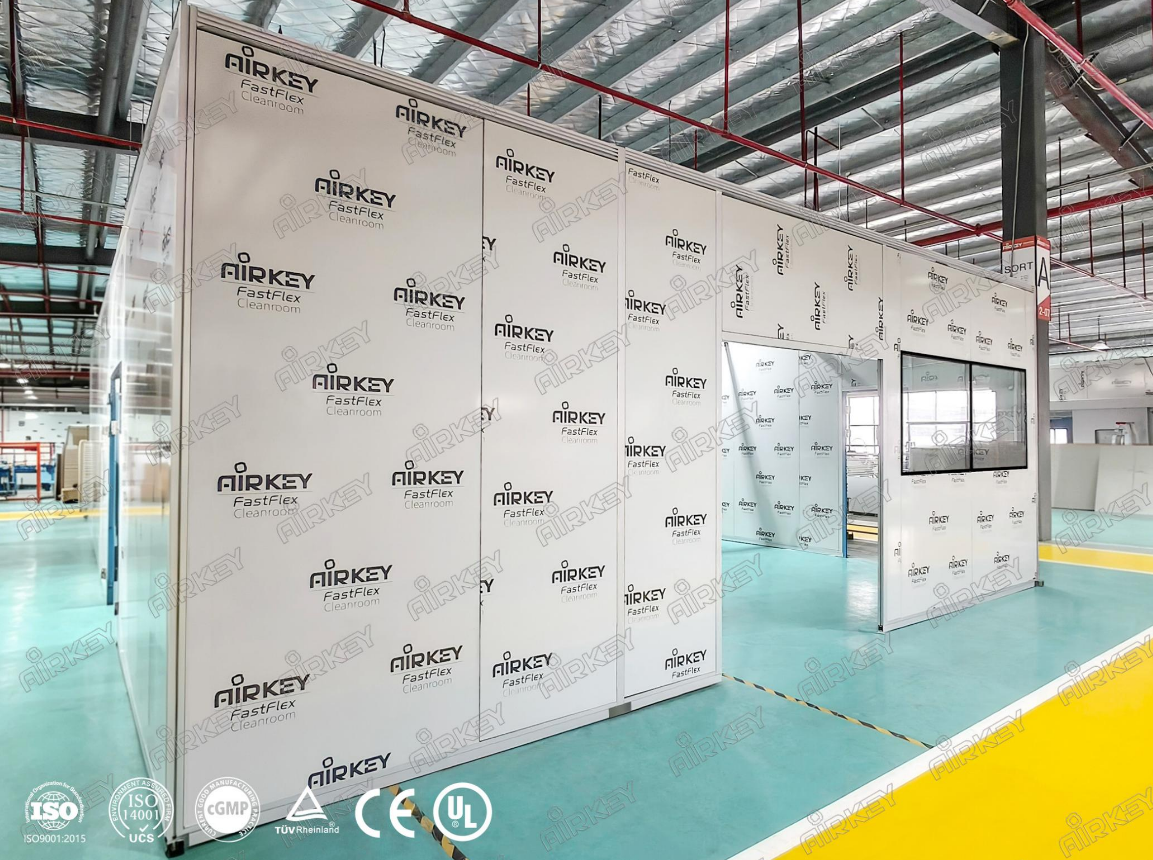
The modular wall system features smooth color-coated steel panels that are easy to disinfect and minimize dust accumulation. Independent positive-pressure and negative-pressure production zones separate reagent preparation, positive control, filling, and packaging processes, effectively preventing cross-contamination throughout manufacturing.
Precision Humidity Control for Stable Production
Humidity control plays a critical role in biological reagent manufacturing, particularly during diagnostic test strip production.
To ensure stable environmental conditions, AIRKEY integrated an independent high-precision dehumidification HVAC system that regulates humidity specifically within core production areas. Instead of upgrading the entire factory, environmental control is applied only where required, significantly reducing operating costs while maintaining optimal production conditions.
This targeted environmental control improves manufacturing stability, enhances product consistency, and delivers substantial energy savings.
Rapid Modular Construction for Faster Production Launch
The modular cleanroom was fully prefabricated at AIRKEY's manufacturing facility before shipment, allowing rapid on-site assembly after delivery.
Compared with conventional cleanroom construction, the modular approach reduced installation time by approximately 40% to 60%, enabling the client to establish its diagnostic reagent production line much faster and respond quickly to increasing market demand.
The modular design also provides excellent flexibility for future production expansion or process modifications without extensive reconstruction.
Large-Span Self-SSupporting Structural Design
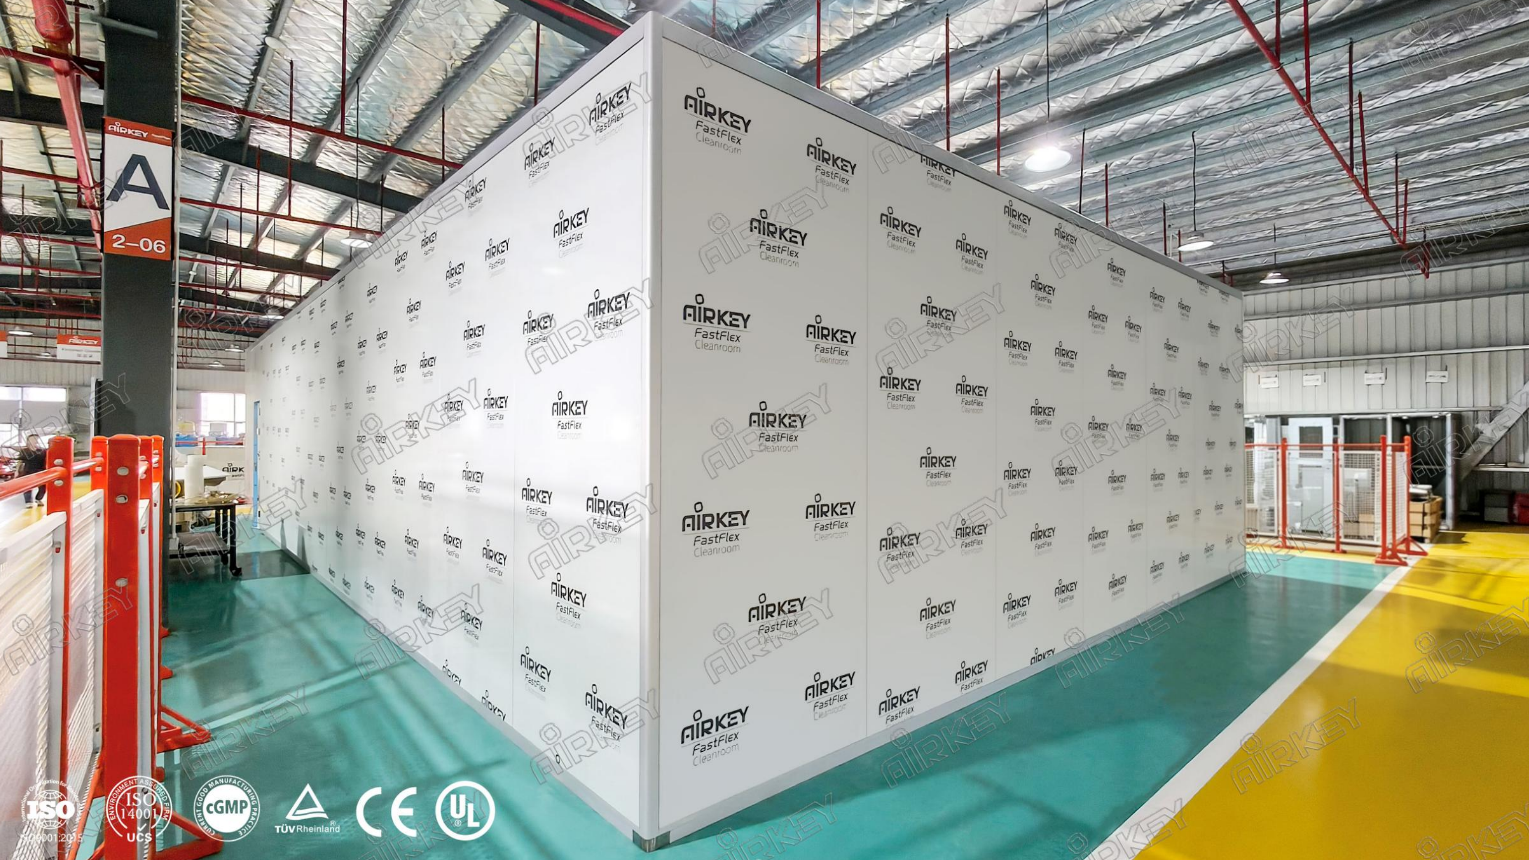
One of the project's most significant engineering features is its large-span self-supporting structure.
The cleanroom measures 27 meters in length with a maximum clear span of 9 meters. AIRKEY's proprietary self-supporting structural system eliminates the need for internal support columns or suspended ceiling brackets, maximizing usable production space and providing greater flexibility for equipment layout and future production line adjustments.
Intelligent Environmental Monitoring System
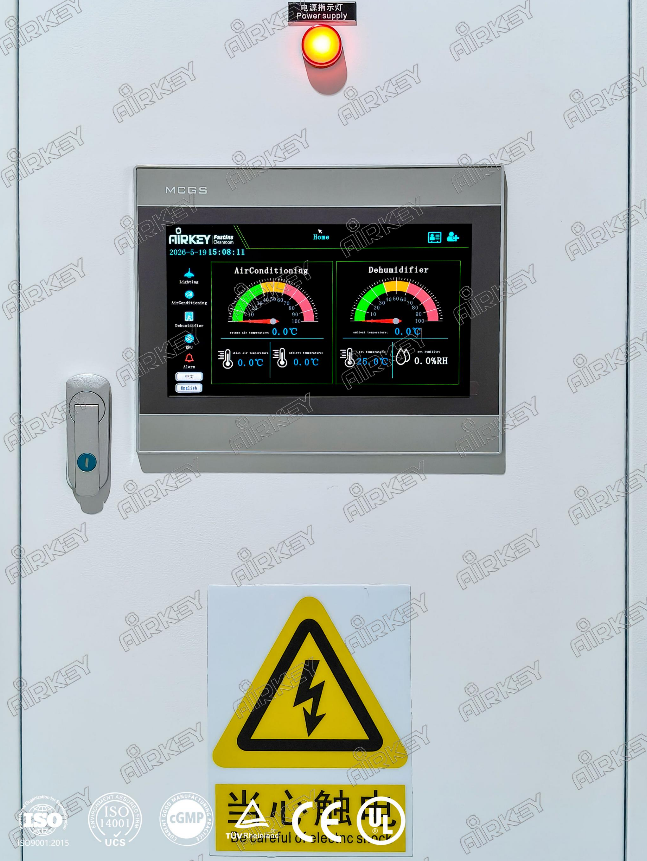
The project incorporates a customized intelligent control system that integrates HVAC equipment and EC Fan Filter Units into a centralized environmental management platform.
Operators can monitor temperature, humidity, airflow, and other environmental parameters in real time through centralized control panels while making immediate adjustments based on production requirements.
The EC FFUs deliver higher airflow efficiency, lower operating noise, and reduced energy consumption, helping maintain stable cleanroom performance while minimizing operating costs.
Pre-Wired Modular Construction for Efficient Installation
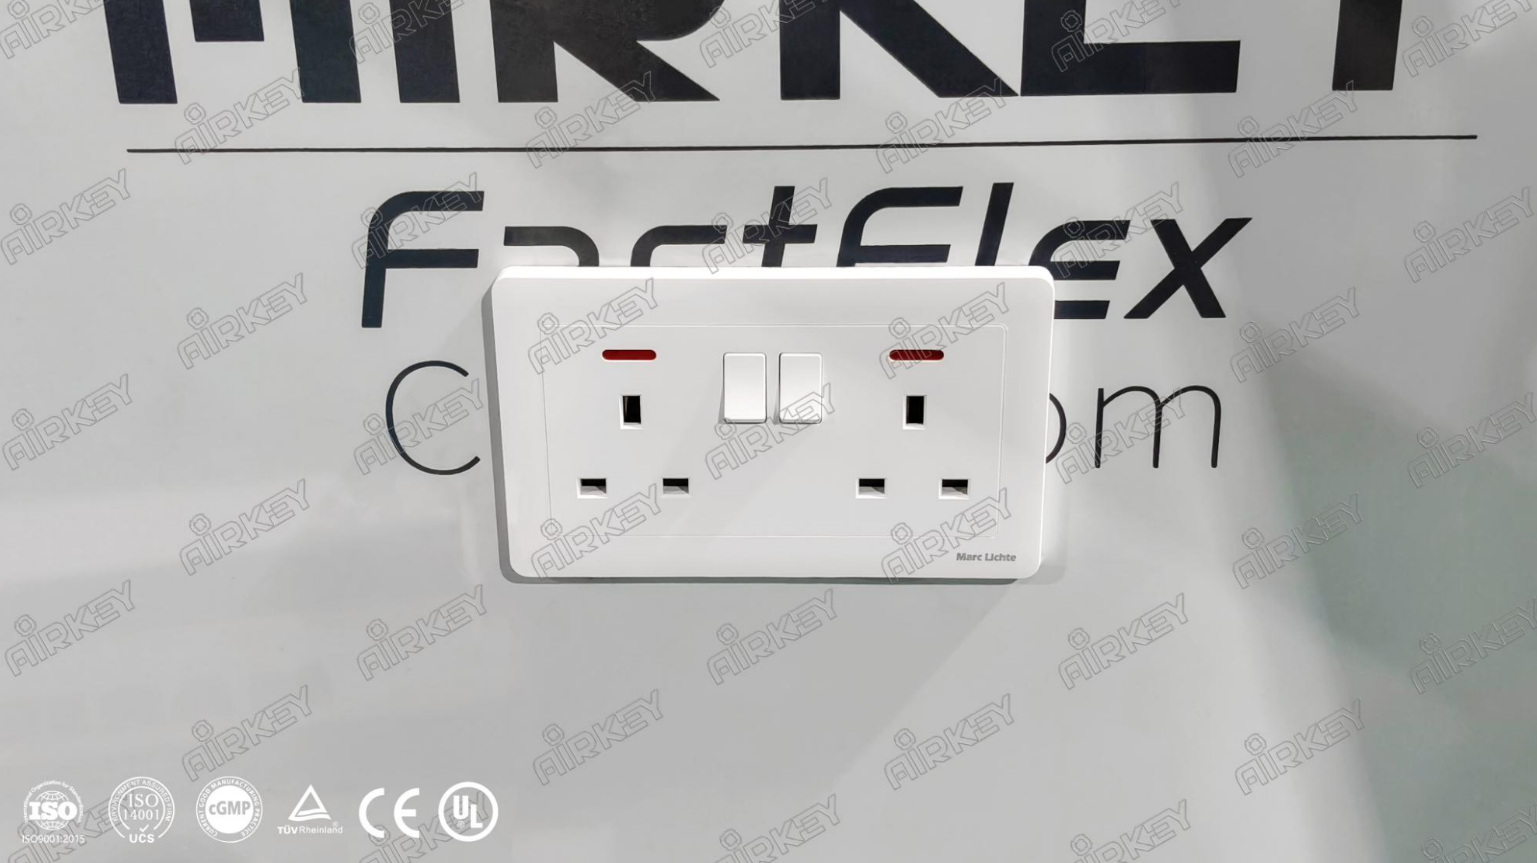
To accelerate project delivery, all electrical wiring was integrated into the modular wall panels during factory production according to the customer's equipment layout.
The cleanroom includes 95 British-standard electrical outlets and multiple network interfaces that were fully pre-installed before shipment. On-site installation required only simple connection to the main electrical distribution system, greatly reducing construction time and improving installation efficiency.
Factory-Tested Performance and Reliable Operation
Every stage of the project, from engineering design and equipment selection to factory manufacturing and on-site installation, followed AIRKEY's strict quality management procedures.
Before shipment, the complete modular cleanroom underwent comprehensive factory testing to verify cleanliness, environmental control, and operational performance. After installation, all performance indicators successfully passed commissioning on the first inspection.
The client personally visited AIRKEY's manufacturing facility for pre-shipment inspection and formally approved the project before delivery, demonstrating confidence in the quality, reliability, and performance of the completed modular cleanroom solution.