Recent Projects
UK Semiconductor ESC Modular Cleanroom Project | ISO 6 & ISO 7 Cleanroom Solution
2026-06-03


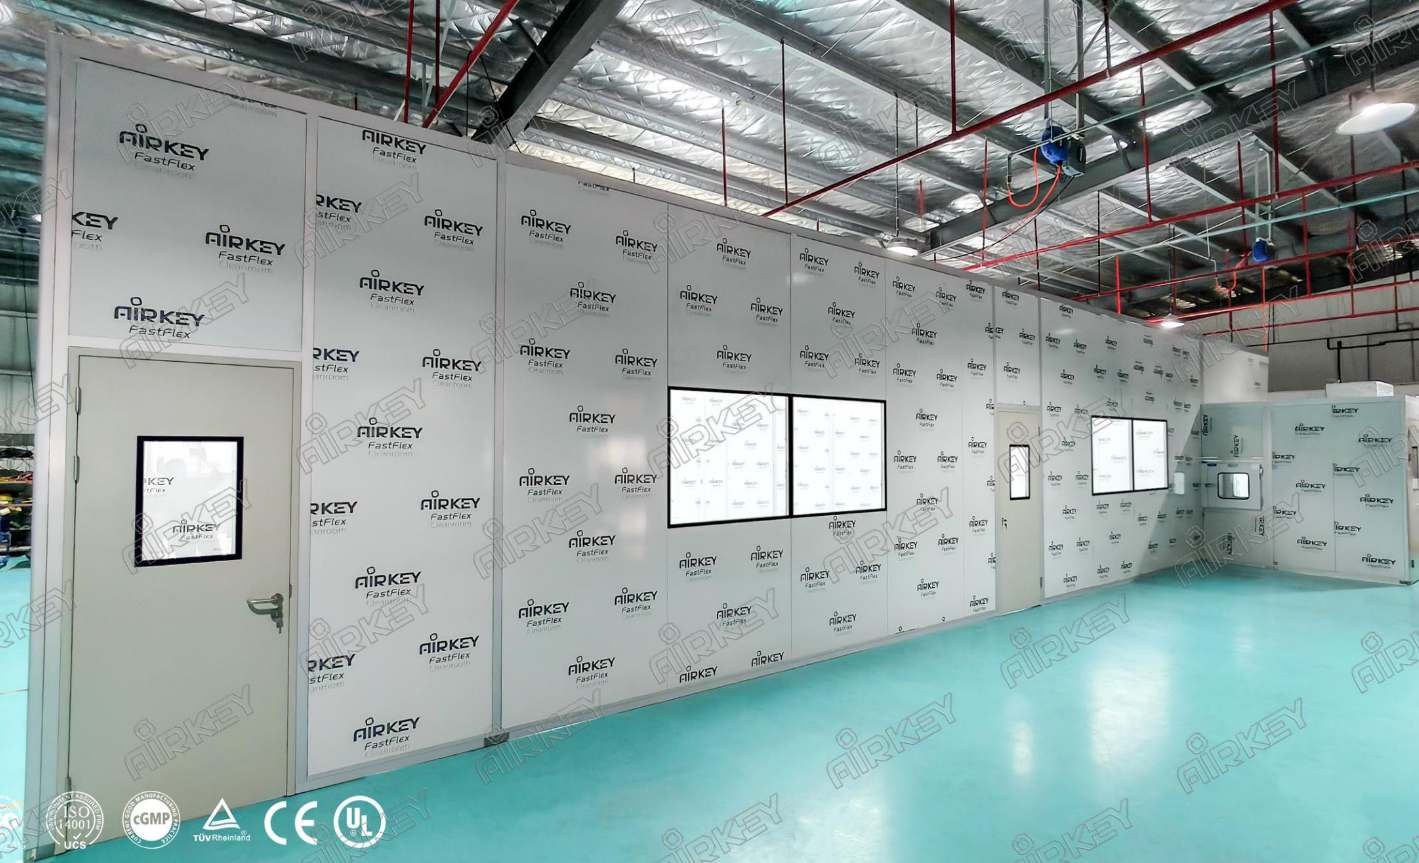
AIRKEY successfully designed and installed a 144㎡ modular cleanroom for a semiconductor chip production facility in Togliatti, Russia. The project was developed to meet the stringent environmental requirements of semiconductor manufacturing, providing a highly controlled production environment that supports product quality, process stability, and manufacturing efficiency.
The cleanroom was built to ISO 8 standards with customized ceiling heights of 2.5m and 3.5m, allowing the modular structure to perfectly fit the client's existing facility while maintaining optimal cleanroom performance.
The client, Sumtech, has more than ten years of experience in the automotive engineering industry and provides comprehensive services covering concept development, engineering design, prototyping, production planning, mass production, and after-sales support.
As the company expanded into semiconductor chip manufacturing, it required a cleanroom capable of maintaining stable environmental conditions throughout every production stage while minimizing contamination risks that could affect chip quality and production yield.
Semiconductor manufacturing is one of the most contamination-sensitive industries. Even microscopic airborne particles can significantly reduce wafer yield and device reliability.
During wafer processing, tiny dust particles or metallic contaminants adhering to wafer surfaces may lead to pattern defects and degraded electrical performance.
In photolithography, airborne particles can damage photoresist patterns and reduce overlay accuracy, directly affecting circuit precision.
During etching and deposition processes, reaction-generated particles that are not removed promptly may redeposit onto wafer surfaces, resulting in uneven film thickness, unstable electrical characteristics, and potential device failure.
Inspection and packaging operations also demand an extremely clean environment. Dust contamination can interfere with optical inspection systems, introduce measurement errors, and reduce testing accuracy before products leave the production line.
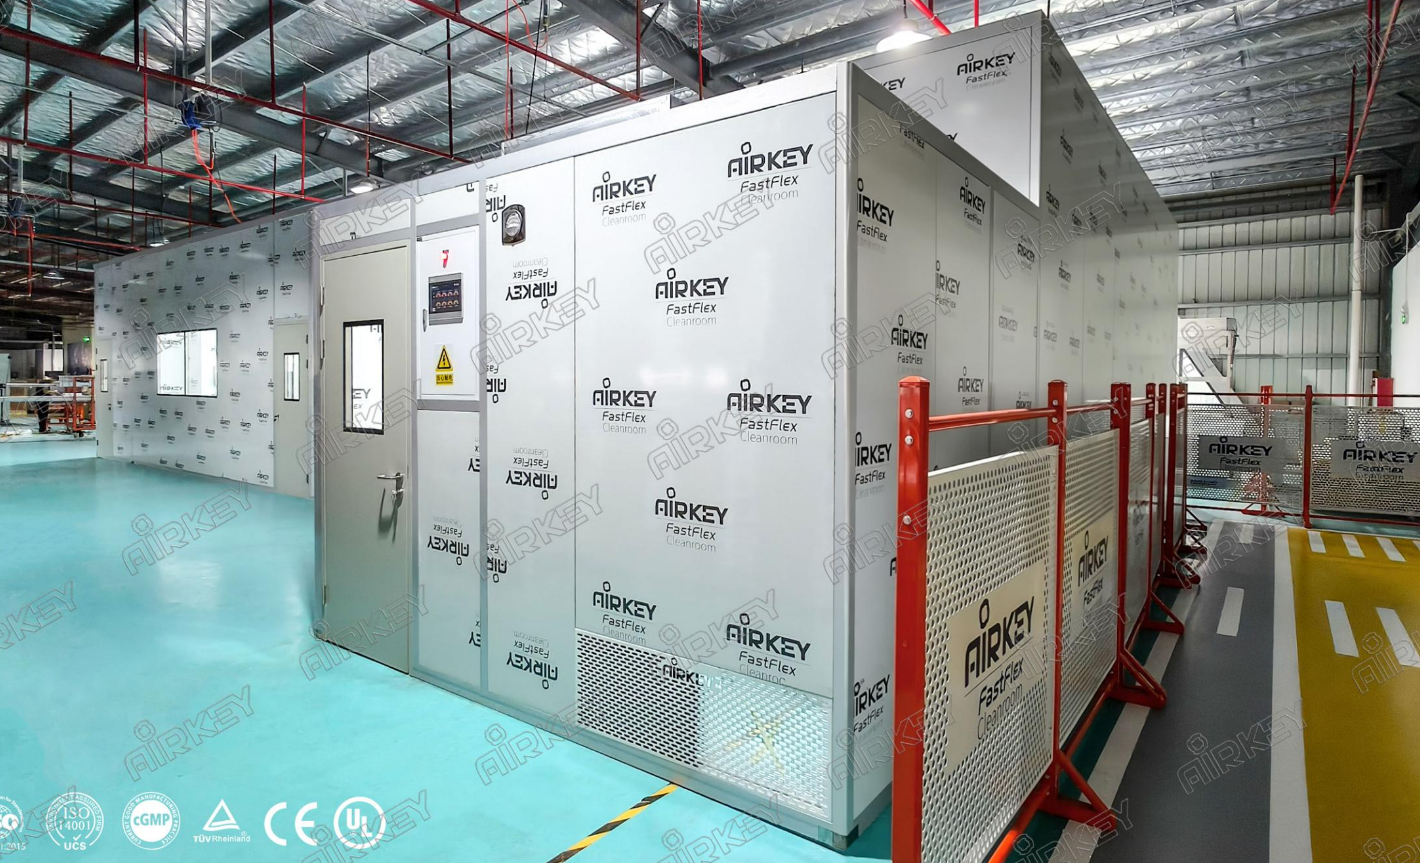
To optimize production workflow and contamination control, AIRKEY designed the modular cleanroom with four dedicated functional areas.
The buffer room serves as the transition area between the external environment and the clean production space. It is equipped with an air shower and pass box to control personnel and material entry while minimizing contamination.
The material preparation room provides a dedicated space for handling production materials before they enter the manufacturing process.
The batching room is designed for intermediate production operations and efficient material transfer.
The main production room accommodates the core semiconductor manufacturing process and includes observation windows, allowing operators to monitor production without disturbing the clean environment.
This well-planned workflow helps separate personnel and material movement, significantly reducing the possibility of cross-contamination.
The client's facility featured two different ceiling heights, creating installation challenges for a conventional cleanroom.
AIRKEY customized the modular cleanroom by lowering the buffer room to 2.5 meters while maintaining a 3.5-meter ceiling in the remaining production areas. This solution enabled the cleanroom to fit perfectly within the existing building layout without compromising cleanroom performance or operational efficiency.
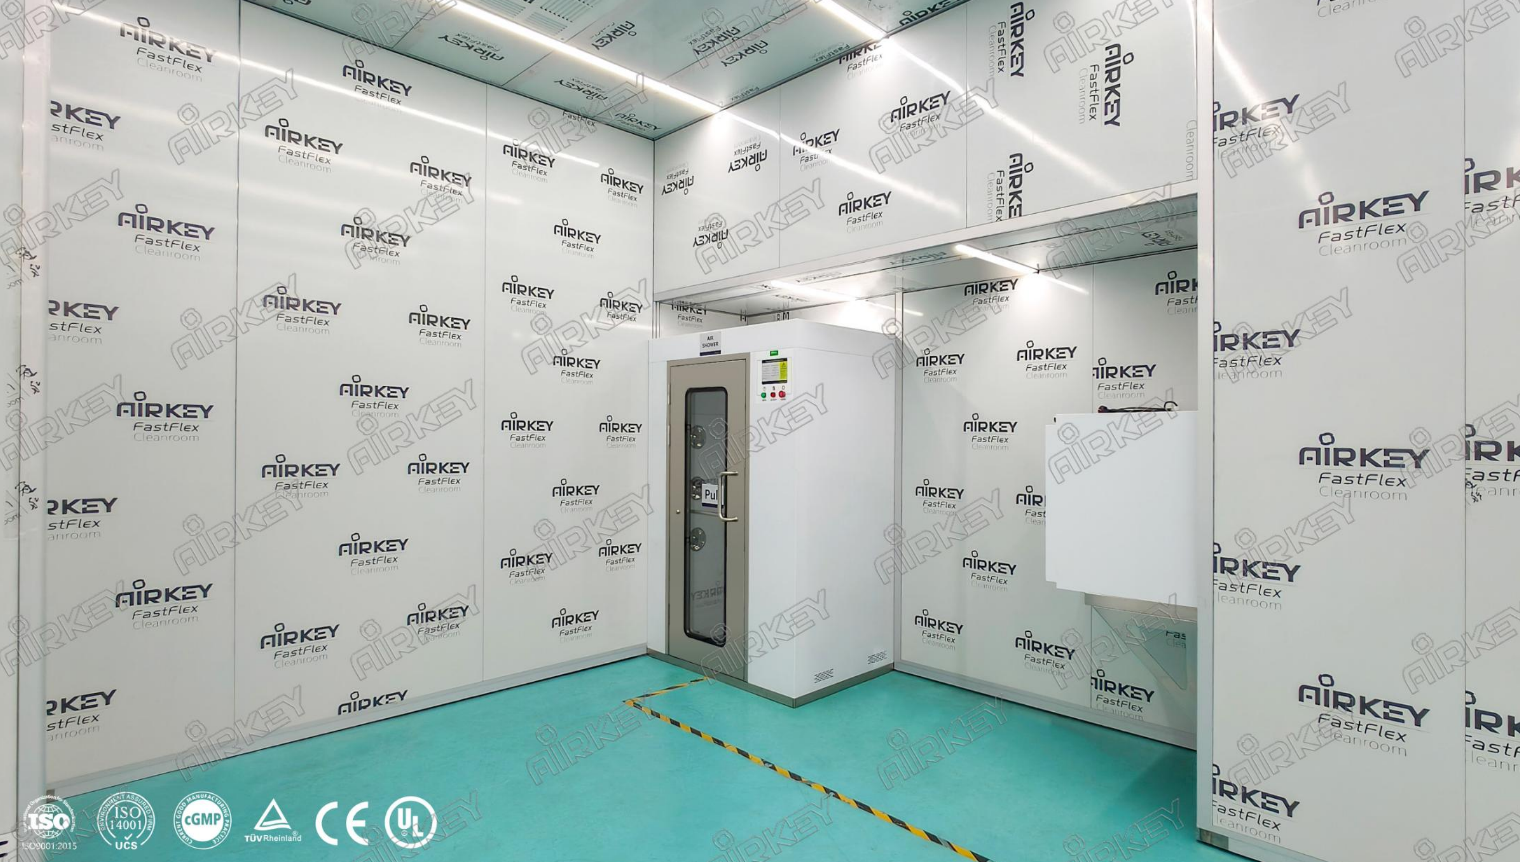
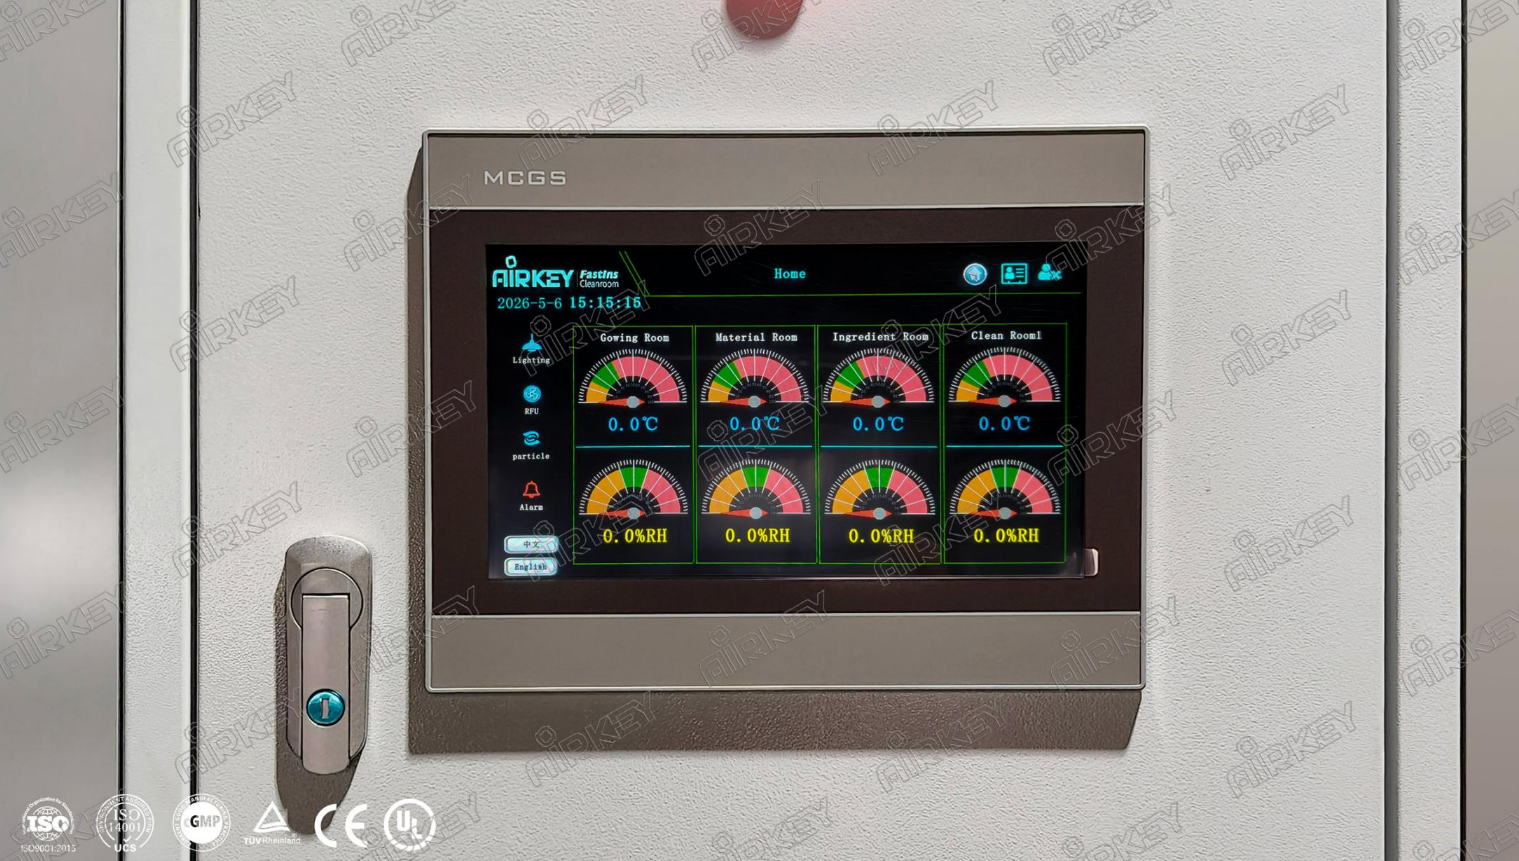
To ensure stable operating conditions, each of the four cleanroom areas is equipped with particle counters as well as temperature and humidity sensors.
All environmental data is transmitted in real time to a custom-programmed central control panel, allowing operators to continuously monitor cleanroom conditions, record historical data, and make immediate adjustments whenever necessary.
The intelligent monitoring system provides precise environmental management while improving operational reliability and regulatory compliance.
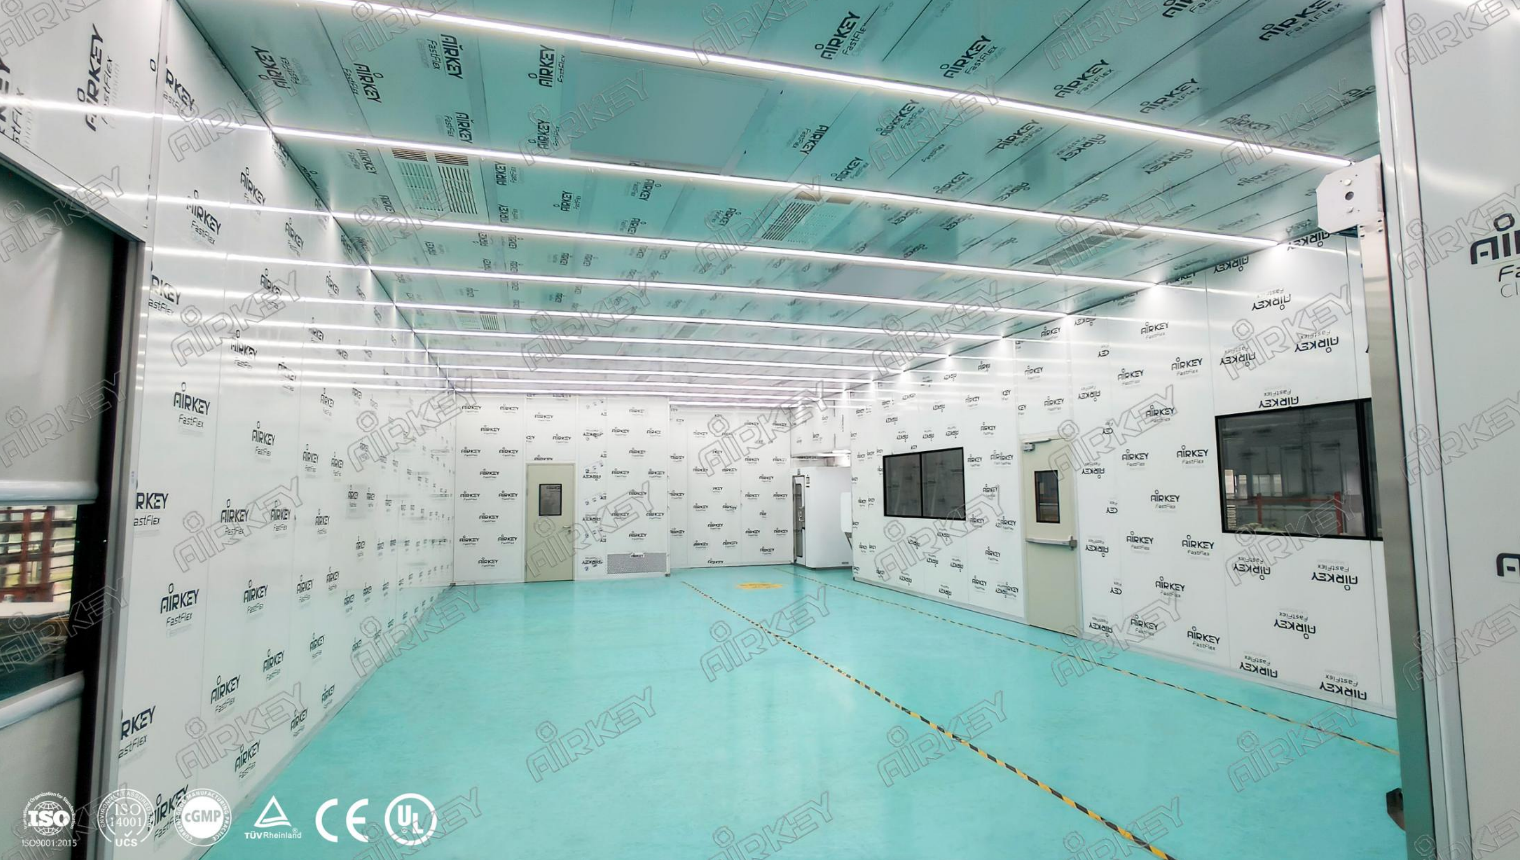
Different production areas require different access solutions. AIRKEY configured multiple door types according to the client's workflow.
The buffer room and material room are equipped with standard single doors for controlled personnel and material access.
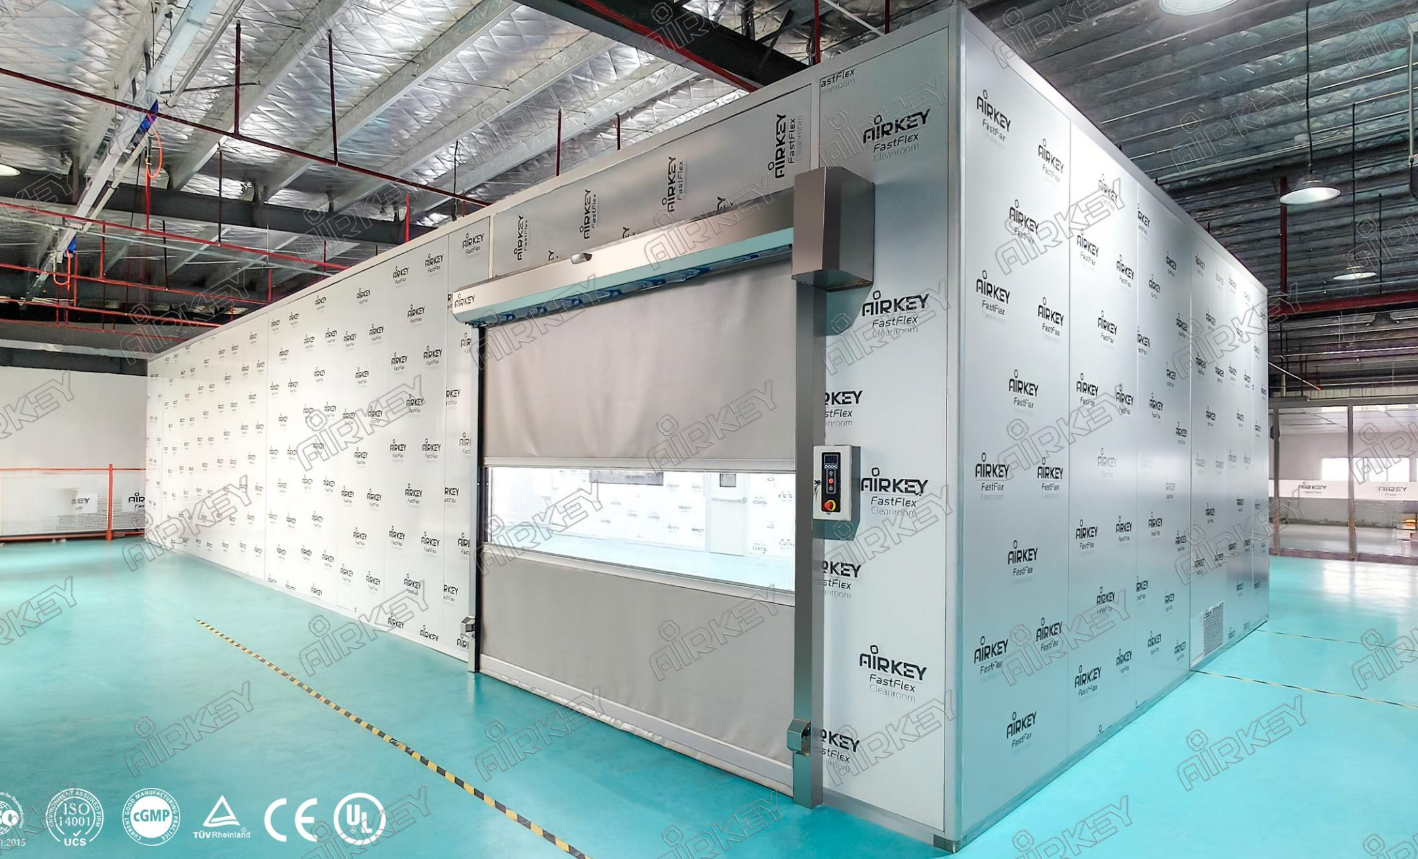
The batching room features two high-speed roll-up doors to support rapid material transfer while maintaining cleanroom pressure stability.
The main production room is equipped with both a large high-speed roll-up door for oversized equipment and an emergency exit door to improve operational flexibility and workplace safety.
This customized door configuration enhances production efficiency without compromising contamination control.
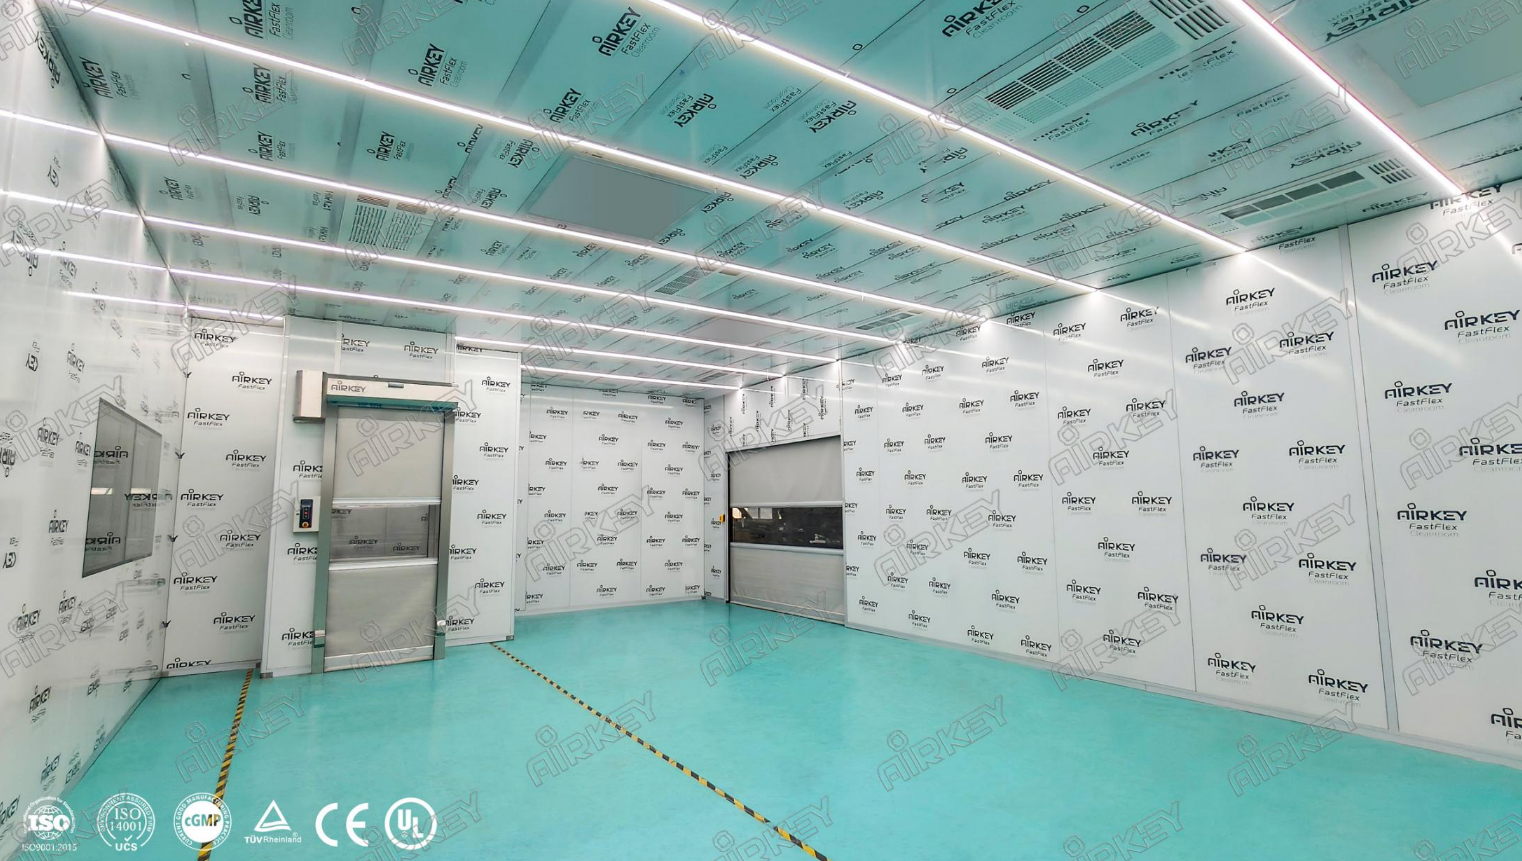
Before shipment, the complete modular cleanroom was prefabricated, assembled, and thoroughly tested at AIRKEY's manufacturing facility.
Key performance indicators, including ISO cleanliness level, temperature control, illumination, and overall system operation, were fully verified before installation. This factory acceptance testing ensured rapid on-site installation and guaranteed that the cleanroom met customer expectations immediately after commissioning.
The completed project provides the client with a reliable, energy-efficient, and scalable cleanroom solution that fully supports the demanding requirements of semiconductor chip manufacturing.